What Is M35 Tool Steel?
Introduction
Molybdenum high-speed steels are designated as Group M steels according to the AISI classification system. Over 95% of high-speed steels manufactured in the US are group M steels. Tungsten is present in all types from M1 to M10, except M6, and cobalt is not present in any of these steels. Molybdenum high-speed steels have similar performance when compared to tungsten high-speed steels. However, the initial cost of molybdenum tool steels is lower. Titanium nitride, titanium carbide and several other coatings can be used in tools made of this kind of steels through physical vapor deposition process to improve the performance and life span of the tool.
Chemical Composition
The following table shows the chemical composition of M35 molybdenum high speed tool steels.
| Element | Content (%) |
| C | 0.93 |
| Cr | 4.2 |
| Co | 4.9 |
| Fe | 76.52 |
| Mo | 5 |
| Si | 0.3 |
| W | 6.25 |
| V | 1.9 |
Physical Properties
| Physical properties | Metric | Imperial |
| Density | 8.14 g/cm3 | 0.294 lb/in3 |
Mechanical Properties
| Mechanical properties | Metric | Imperial |
| Hardness, Rockwell C (oil quenched from 1232°C, 5 mins) | 64.8 | 64.8 |
| Hardness, Rockwell C (oil quenched from 1177°C, 5 mins) | 65.2 | 65.2 |
| Hardness, Rockwell C (oil quenched from 1204°C, 5 mins) | 65.2 | 65.2 |
| Modulus of elasticity | 207 GPa | 30000 ksi |
| Machinability (1% carbon steel) | 45.0 – 50.0% | 45.0 – 50.0% |
Thermal Properties
| Thermal properties | Metric | Imperial |
| CTE, linear (@21 – 399°C / 69.8 – 750°F) | 11.4 μm/m°C | 6.33 μin/in°F |
| CTE, linear (@21 – 593°C /69.8 – 1100°F) | 11.5 μm/m°C | 6.39 μin/in°F |
The middle of the cobalt range
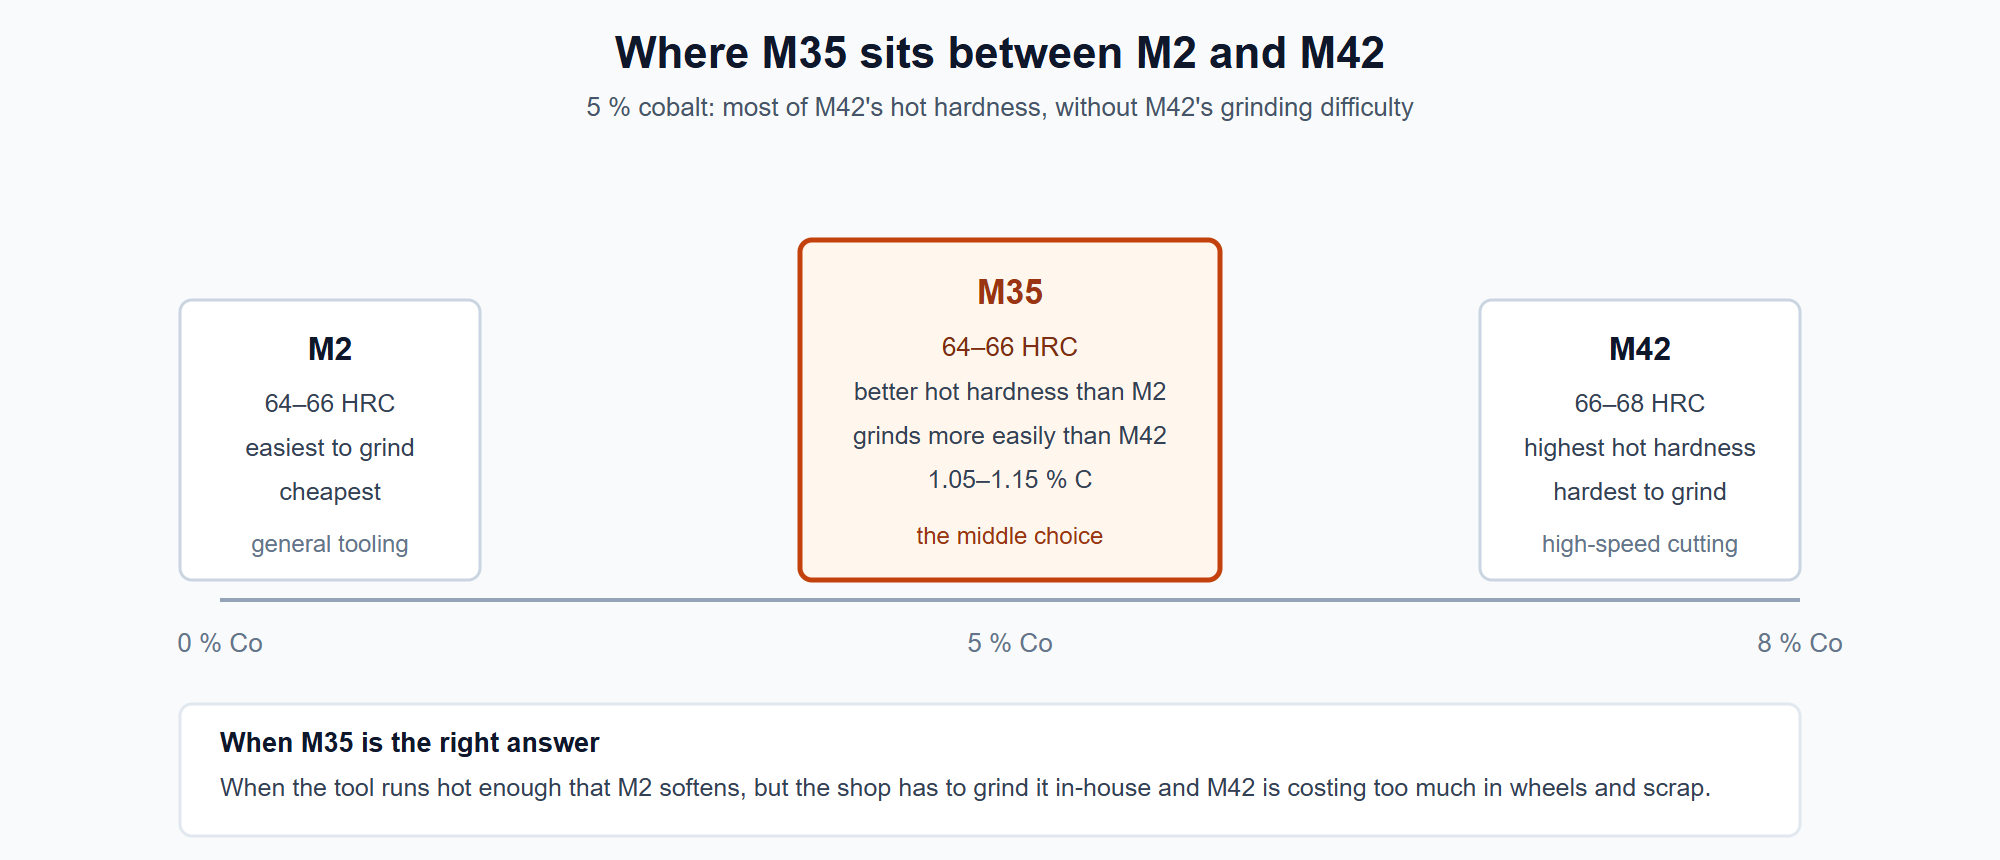
M35 carries about 5 % cobalt, between M2 at none and M42 at 8 %. It hardens to 64–66 HRC and holds that hardness about 20 °C higher than M2 in continuous cutting.
That sounds marginal until the tool is running hot: 20 °C is often the difference between an edge that lasts a shift and one that has to be changed mid-run.
Why not just buy M42
Grindability. M42 at 8 % cobalt and higher carbon is noticeably harder to grind, and a shop without the right wheels loses the benefit in tool room time and scrap. M35 gives most of the hot hardness with a grinding behaviour closer to M2.
For a shop that buys tools finished, M42 is usually the better buy. For a shop that grinds its own, M35 is often the practical compromise.
Typical uses
Drills and taps run at moderate speed in tough alloys, milling cutters, and broaches — tools where the heat is real but the cutting speed is not extreme.