Inconel 725 (UNS N07725): Age-Hardenable Nickel Alloy
An age-hardenable nickel–chromium–molybdenum alloy with niobium and titanium. It corrodes like 625 and yields at 827 MPa — which is why it is specified for sour-gas downhole hardware that has to carry load in a chloride environment.
Alloy 725 was developed to solve a specific problem: 625 has the corrosion resistance the oil patch wants, but in the annealed condition it yields at only about 414 MPa, and the usual way of raising that — cold working — does not work on a 200 mm forged hanger or a thick-wall connector. 725 gets its strength from a precipitation reaction instead, so the whole section hardens uniformly, whatever its shape.
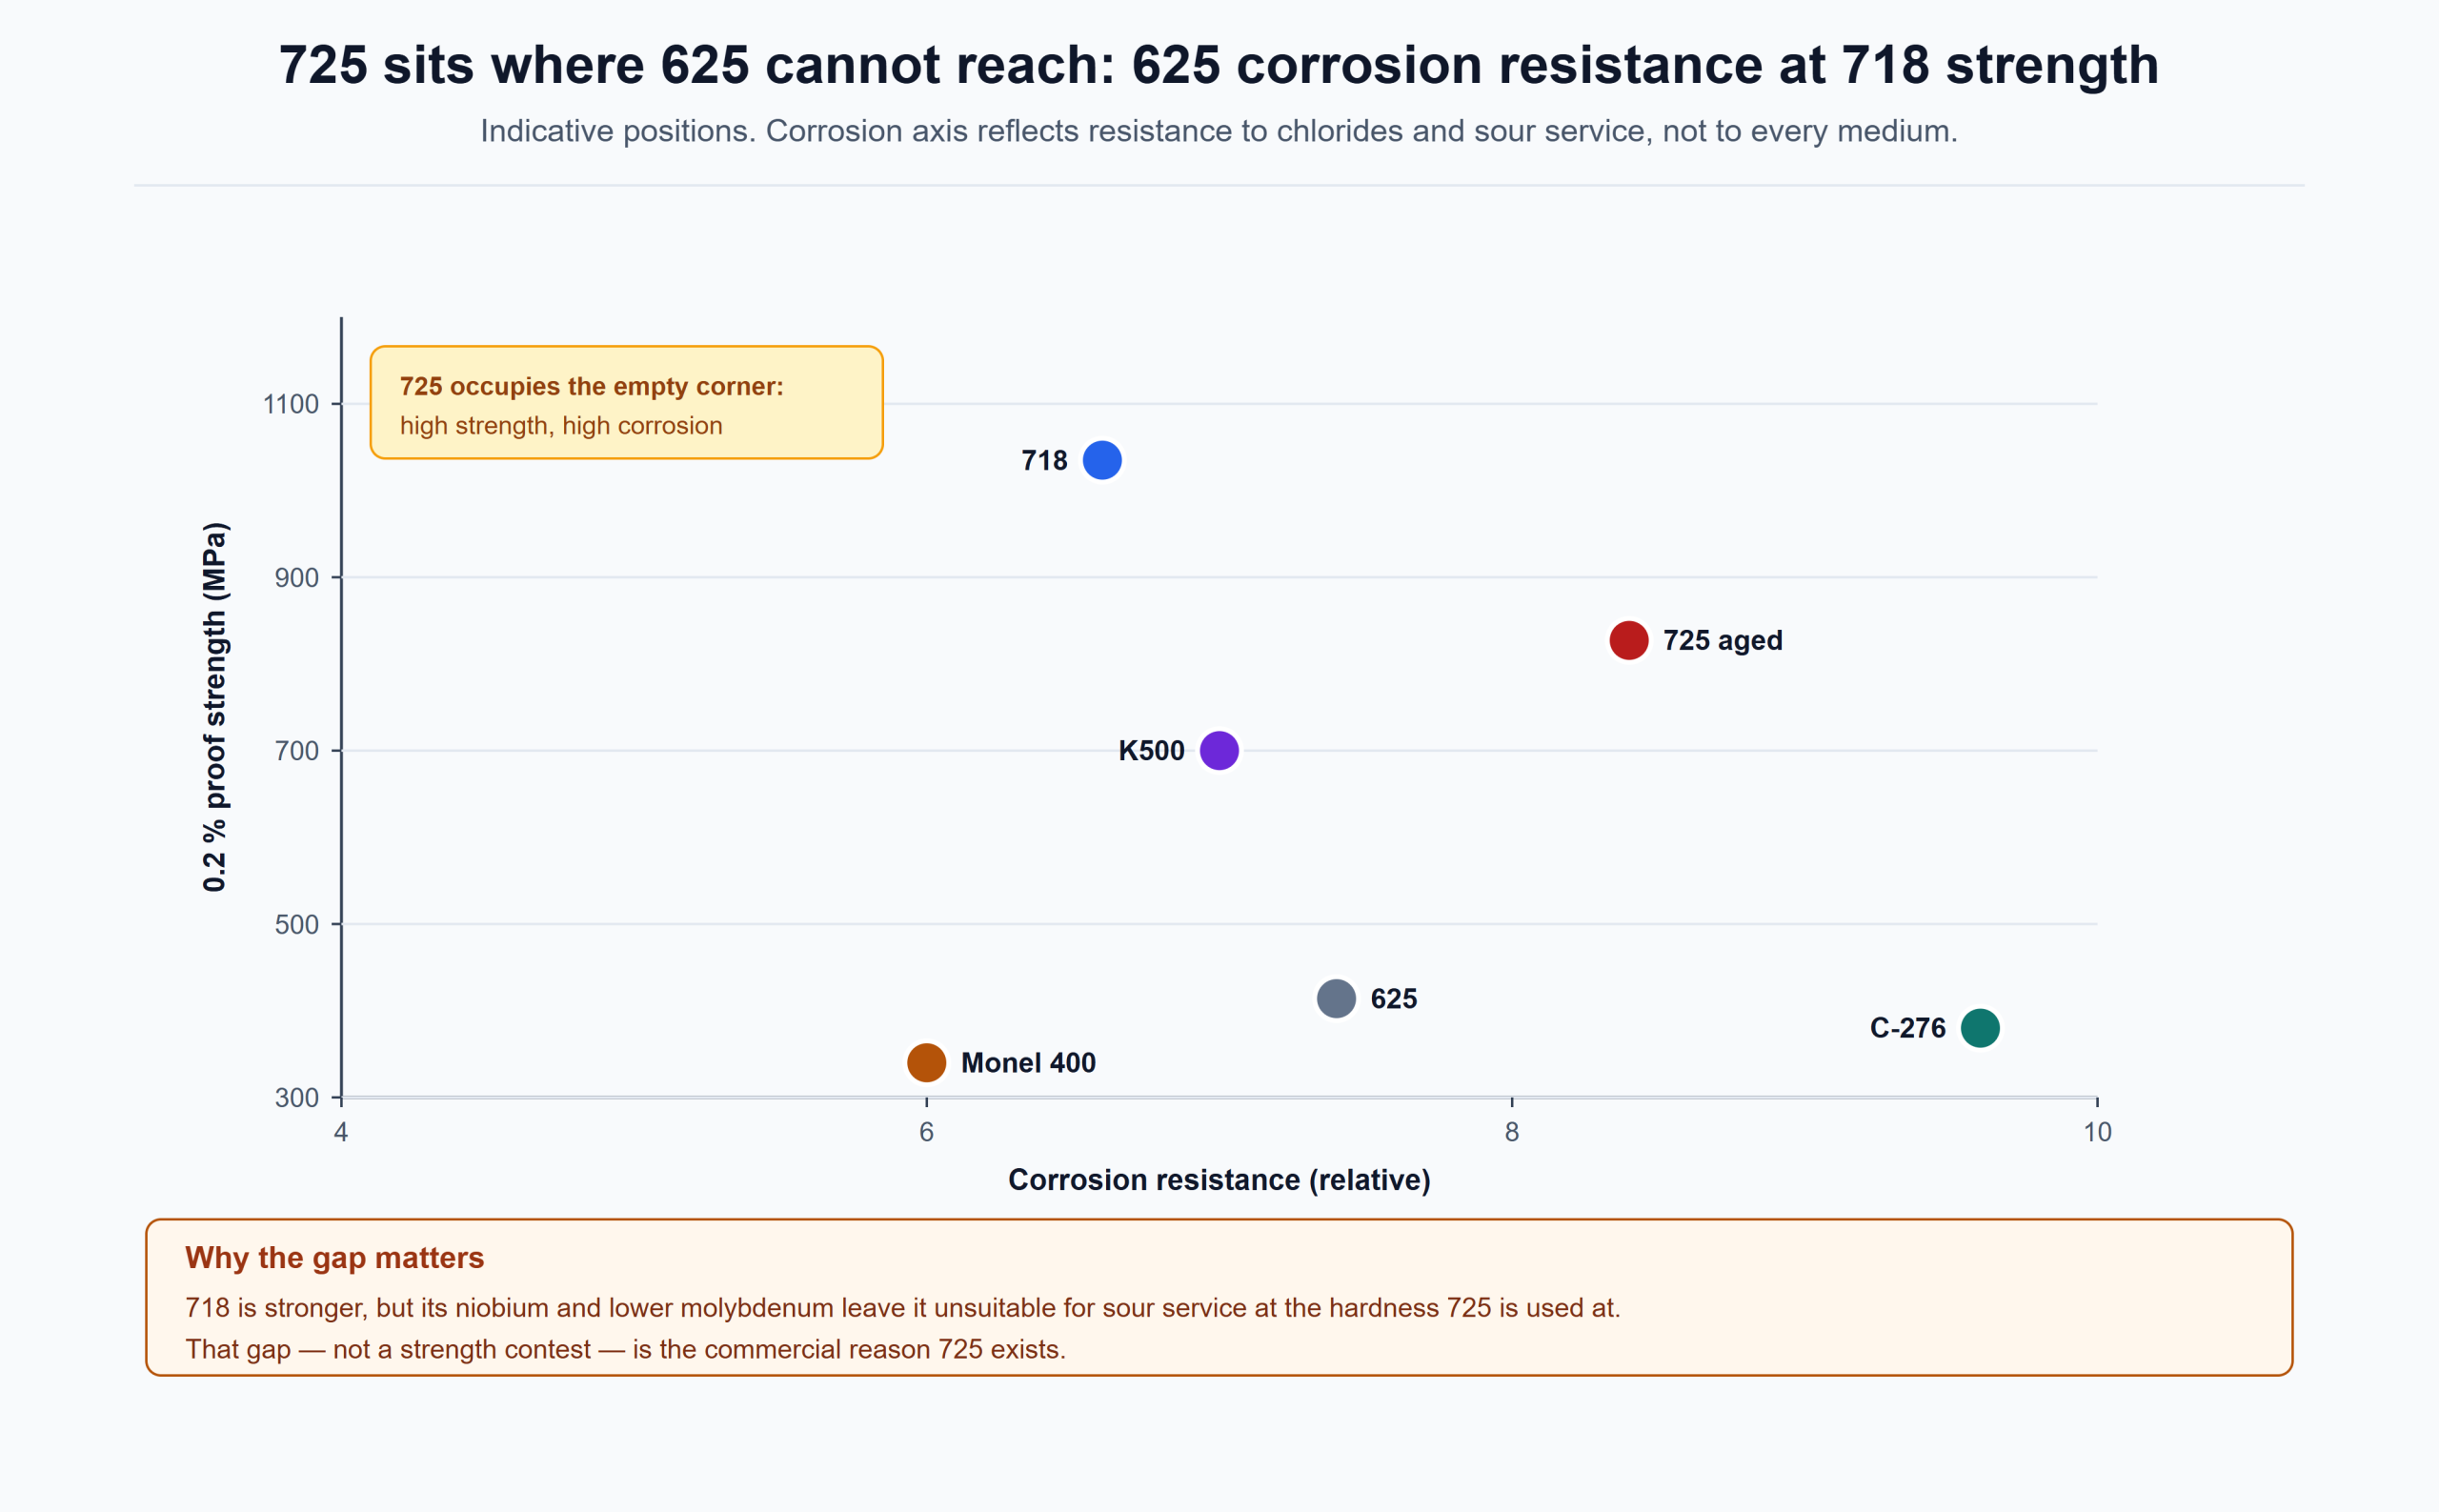
The result is roughly twice the yield strength of annealed 625, with the same corrosion behaviour, and it is approved for sour service under NACE MR0175 / ISO 15156. In practice 725 is bought for downhole tubulars, hangers, connectors, valve stems and fasteners where 718 would be strong enough but not corrosion resistant enough, and 625 would be corrosion resistant enough but not strong enough.
What ageing does
725 is solution annealed at about 1040 °C, which puts the alloying elements into solid solution and leaves a soft, ductile matrix. The part is machined in that condition, then aged in two steps: hold at about 732 °C, cool slowly to 621 °C, hold again, and air cool. During the hold, the niobium and titanium combine with nickel to precipitate γ″ (Ni3Nb) particles, and those particles block dislocation motion. That is the whole strengthening mechanism.
Because it is a bulk reaction rather than a surface one, the strength is uniform through the section — the advantage over cold work, which fades towards the centre of a thick bar. The trade is that the ageing treatment has to be done after machining, and a part that is subsequently welded needs the heat treatment repeated.
Strength against the grades it competes with
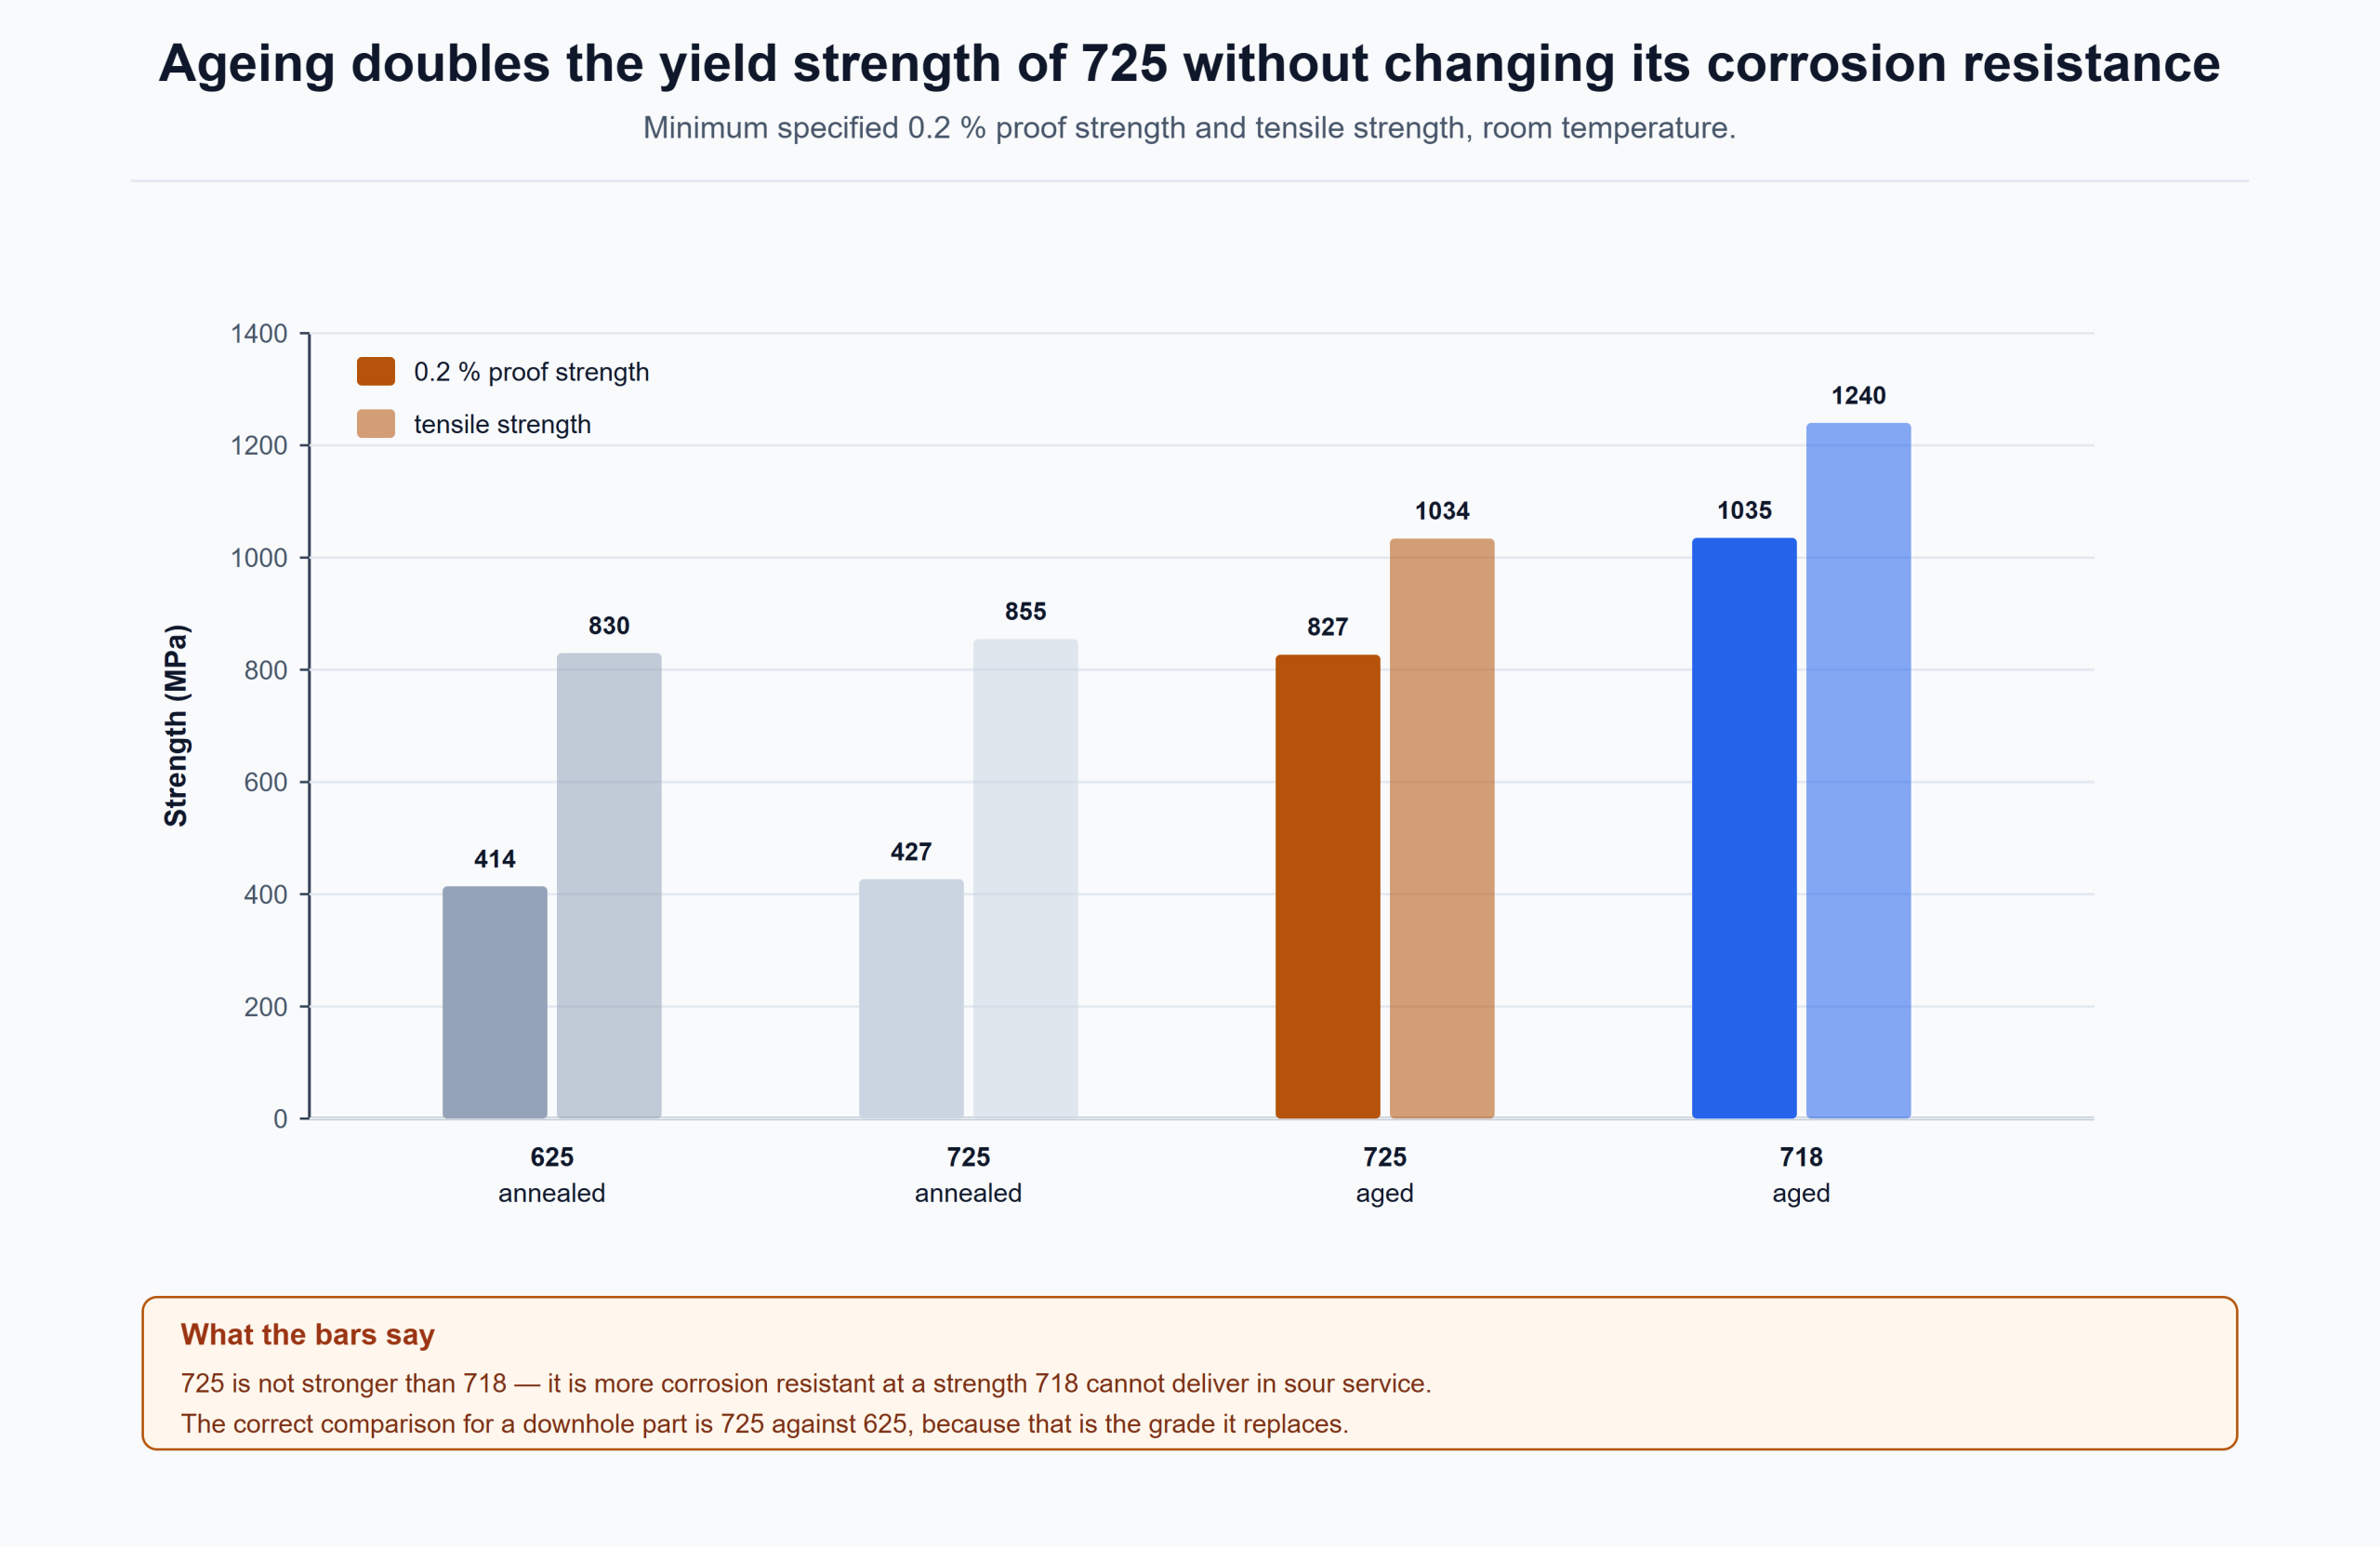
The comparison that matters is with 625 and 718. Against 625 annealed, 725 doubles the yield strength with the same corrosion resistance. Against 718 aged, 725 gives up about 20 % of the yield strength but keeps substantially better resistance to chlorides and to sour service — 718 is not approved for the same environments at the same hardness.
Chemical composition
Table 1. Chemical composition of Inconel 725 (UNS N07725), mass fraction in percent. Nickel balance.
| Ni | Cr | Fe | Mo | Nb | Ti | Al | C |
|---|---|---|---|---|---|---|---|
| 55.0–59.0 | 19.0–22.5 | ≤9.0 | 7.0–9.5 | 2.75–4.0 | 1.0–1.7 | ≤0.35 | ≤0.030 |
The niobium and titanium are the age-hardening elements and their ratio matters: they are balanced so that the γ″ phase forms rather than the coarser, less effective δ phase. That balance is why 725 is not a grade to buy on a chemistry approximation, and why the certificate should be read against the specification rather than against a generic “Ni-Cr-Mo” description.
Mechanical properties
Table 2. Minimum mechanical properties of 725 in the annealed and aged conditions, bar and forgings to about 250 mm.
| Property | Annealed | Aged |
|---|---|---|
| 0.2 % proof strength | 427 MPa | 827 MPa |
| Tensile strength | 855 MPa | 1034 MPa |
| Elongation | 57 % | 20 % |
| Reduction of area | — | 35 % |
| Hardness | about 5 HRC | <43 HRC |
| Charpy V at −60 °C, longitudinal | — | 54 J average, 47 J minimum |
| Charpy V at −60 °C, transverse | — | 50 J average, 43 J minimum |
Two numbers in that table are worth pausing on. The aged hardness is specified as a maximum (<43 HRC) because NACE MR0175 limits hardness in sour service, and a heat that comes out harder has to be re-aged rather than used. And the impact values are measured at −60 °C, which is the qualification temperature for subsea and cold-climate hardware, not a room-temperature formality.
Physical properties
Table 3. Physical properties at room temperature.
| Property | Value |
|---|---|
| Density | 8.31 g/cm³ |
| Melting range | 1271–1343 °C |
| Young’s modulus | 204 GPa |
| Poisson’s ratio | 0.31 |
| Specific heat at 20 °C | 0.43 J/g·K |
| Electrical resistivity at 20 °C | 1.144 µΩ·m |
| Thermal conductivity at 20 °C | 10.6 W/m·K |
| Mean CTE, 20–100 °C | 13 × 10-6/K |
| Magnetic permeability at 20 °C | <1.001 |
Corrosion and sour service
The corrosion resistance is essentially that of 625, and it comes from the same three elements. Nickel at 55–59 % ensures resistance to stress-corrosion cracking in chlorides. Chromium at about 21 % handles oxidising conditions such as nitric acid. Molybdenum at 8 % handles reducing conditions such as sulphuric and phosphoric acid, and resists pitting and crevice attack. Niobium and titanium inhibit intergranular corrosion.
The combination is what makes the grade suitable for wells containing CO2, chlorides and H2S together — the classic sour-gas condition. Approval under NACE MR0175 / ISO 15156 is for the aged condition at controlled hardness; it is not a blanket approval for any heat treatment or any hardness, and the certificate has to state the condition.
Where it is used
- Downhole tubulars and completion equipment for sour service.
- Hangers, connectors and subsea hardware where a thick section has to be strong throughout.
- Valve stems, seats and bodies in chloride-bearing process streams.
- High-strength fasteners for marine and offshore structures.
- Chemical process equipment: agitators, pump shafts, heat-exchanger components.
Heat treatment
Solution anneal at 1040 ±15 °C, then cool rapidly enough to keep the carbides and γ″ in solution. Age at 732 °C for 8 hours, furnace cool to 621 °C, hold 8 hours, air cool. Both steps are usually done under a protective atmosphere or in vacuum on finished parts, and the ageing treatment is repeated after any welding that is not subsequently solution annealed.
The two-step age is not optional. A single hold at the higher temperature produces an under-aged structure with lower strength; a single hold at the lower temperature produces a coarse precipitate that never reaches the specified proof stress.
Supply range and condition
Table 4. Forms and conditions available.
| Form | Condition | Note |
|---|---|---|
| Bar and billet | Solution annealed, or annealed and aged | Ø12–300 mm; cut lengths and forged blanks |
| Seamless tube and pipe | Solution annealed | Downhole and instrumentation sizes |
| Welded tube | Solution annealed | Larger diameters and thin wall |
| Forgings | Solution annealed, or annealed and aged | Hangers, connectors, valve bodies to drawing |
| Wire and rod | Solution annealed | For fasteners and weld consumables |
| Sheet and plate | Solution annealed | Thin sections and liners |
| Fittings, flanges and weld rod | Solution annealed, or aged | To the matching ASTM product specification |
Table 5. Testing and certification for 725.
| Test | Standard | When it is required |
|---|---|---|
| Chemical analysis | ASTM E1473 / product spec | Every heat |
| Tensile at room temperature | ASTM A370 | Every heat treatment batch |
| Tensile at temperature | ASTM A370 | When the design uses elevated-temperature allowables |
| Hardness survey | ASTM E18 | Every batch for sour service; HRC <43 |
| Impact at −60 °C | ASTM E23 | Subsea and cold-climate hardware |
| Ultrasonic or penetrant test | ASTM A388 / E165 | Bar and forgings for pressure duty |
Certification is to EN 10204 3.1, with the chemistry, the heat-treatment record and the mechanical properties at temperature where required. For sour service the certificate must also carry the hardness survey and the NACE MR0175 statement, and the ageing treatment has to be traceable to the batch.
Inspection, certification and services
Every incoming lot is visually inspected and PMI tested before processing; finished parts are checked dimensionally, by PMI and by hardness before despatch. Where the part is welded after ageing, the age is repeated and the certificate reissued — the properties are not recoverable without it.
Table 6. Workshop and commercial services offered with Inconel 725.
| Service | Detail |
|---|---|
| Cutting | Saw-cut blanks; waterjet cut plate to drawing |
| Machining | CNC turning, milling and thread milling in the solution-annealed condition |
| Heat treatment | Solution annealing and the two-step age, in vacuum or protective atmosphere |
| Packing | Bare, nylon wrap, wooden case; export seaworthy packing |
| Payment and terms | T/T, L/C at sight, or O/A against approved credit; FOB, CFR, CIF, DDU or DDP |
What to put on the enquiry
- Grade and UNS number: Inconel 725, UNS N07725 — and whether the part is for sour service.
- Condition: solution annealed for machining, or solution annealed and aged to the specified proof stress.
- Section size, because the ageing response and the achievable properties depend on it.
- Test requirements: tensile at room temperature, impact at −60 °C, hardness survey, and any third-party witness.
Related reading
- Inconel 625 — the alloy 725 was derived from, and the corrosion baseline
- Inconel 718 — higher strength, lower chloride resistance; the usual alternative
- Hastelloy C-4 — the step up in corrosion resistance when 725 is not enough
- Monel K500 — the age-hardenable nickel–copper option for marine hardware
- Hastelloy C-2000 — the most corrosion-resistant option in the family
You get chemical composition, mechanical properties and a price — with inspection certificates to EN 10204 3.1 issued against the heat number.