
AISI 4317 Alloy Steel: Chemistry & Heat Treatment
AISI 4317 is a nickel-chromium-molybdenum carburising steel with a 0.15–0.21 % carbon core. It is the American counterpart of 18CrNiMo7-6, and it is chosen for gears and shafts where the case has to reach 60 HRC while the core stays at 1,000 MPa and 60 J — the balance that a plain chromium steel cannot hold in a 50 mm section.
Where AISI 4317 Fails — and Why
The grade is bought on its hardenability band. Nickel at 1.4–1.7 % and molybdenum at 0.25–0.35 % push the band far enough that a 30 mm gear blank through-hardens in oil after carburising; a 16MnCr5 blank of the same size does not. That is the difference the drawing is paying for, and it is why the grade is common in gearboxes and wind-turbine gearing.
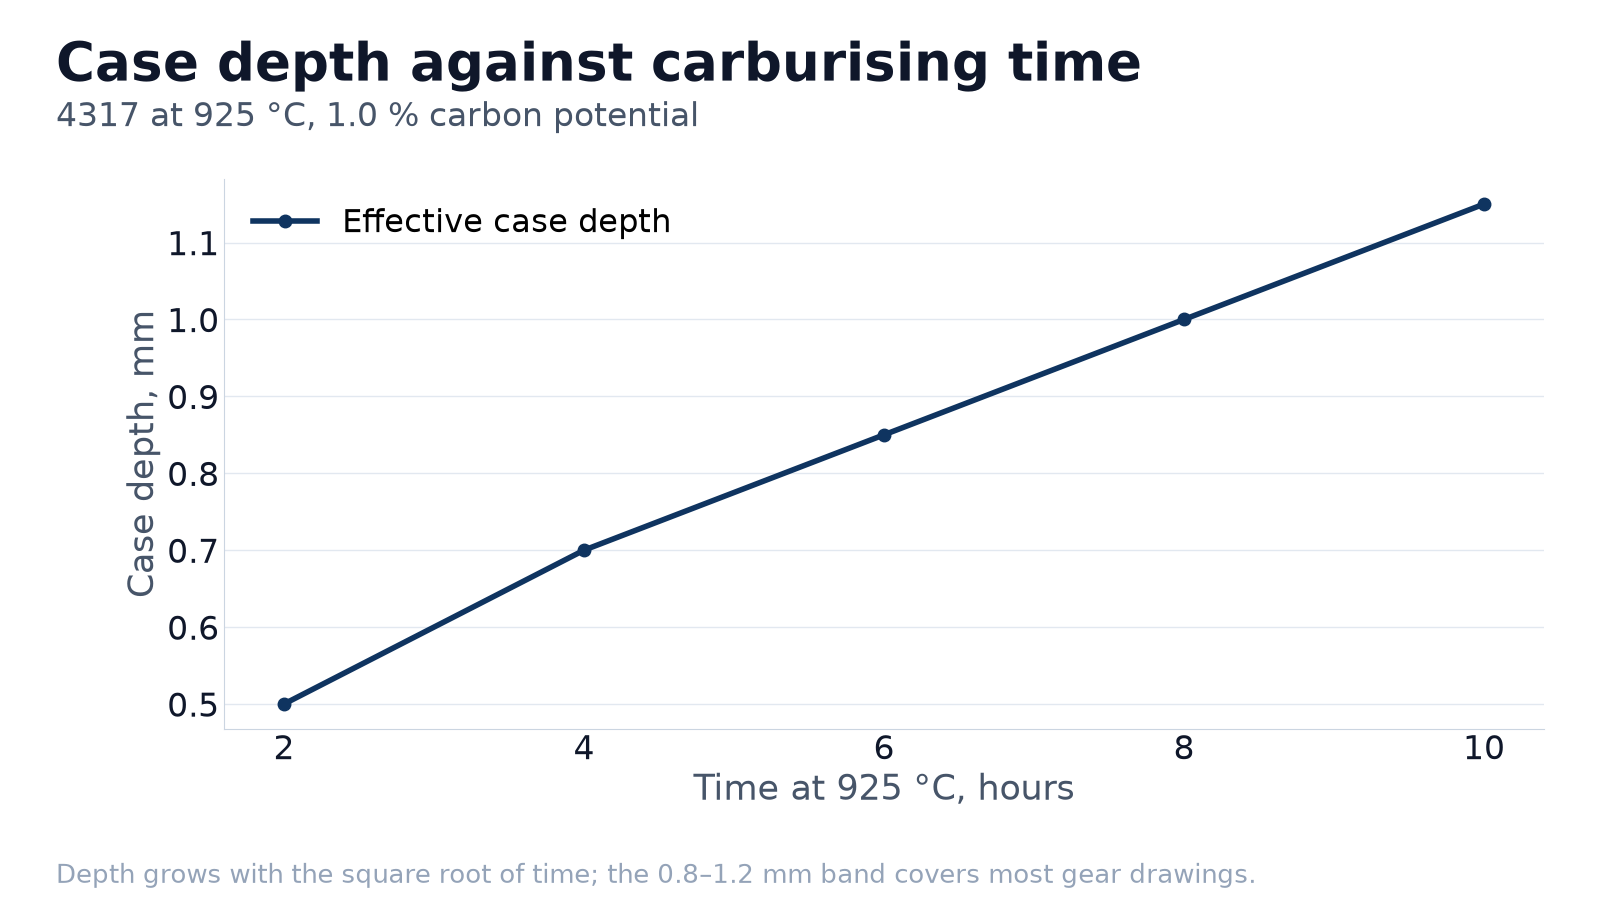
The heat treatment is a three-step sequence: carburise at 900–930 °C, quench from 830–850 °C, temper at 150–200 °C. The temper is low because the case has to stay at 58–62 HRC; the core toughness comes from the nickel, not from a higher temper.
AISI 4317 is a case-hardening steel: a low-carbon core that stays tough, and a carburised surface that carries the wear. The part is machined soft, carburised, quenched and tempered, and the case depth is designed against the contact stress rather than picked from a catalogue.
The chemistry is built for that split. Low carbon keeps the core ferritic and tough; chromium and molybdenum give the case its hardenability so that it does not turn into pearlite during the quench; nickel, where present, improves the core toughness at the same strength.
The process window is where most problems occur. Carburising temperature sets the case depth and the grain growth; the quench decides whether the case is fully martensitic; the temper decides whether the surface is tough enough to resist chipping. Each of the three can be varied, and each moves the fatigue result.
- Specifying case depth without the tolerance; effective case depth and total case depth are different measurements and are not interchangeable.
- Carburising at too high a temperature for too long; the grain coarsens and the core toughness falls away.
- Quenching from the carburising heat without controlling the case austenite; retained austenite shows up as a soft skin after grinding.
- Grinding through the case; the part then has the wear resistance of the core, and the failure appears in service rather than at inspection.
How AISI 4317 Compares
The European and American versions are close enough to quote against each other, but the phosphorus and sulphur limits differ, so a drawing that names one should not be supplied with the other without a written concession.
Table 1 — AISI 4317 against the carburising grades it is usually specified with
| Grade | Core carbon | Ni | Case/core balance |
|---|---|---|---|
| 4317 | 0.15–0.21 % | 1.40–1.70 % | Tough core, deep case |
| 4320 | 0.17–0.22 % | 1.65–2.00 % | Higher core strength |
| 18CrNiMo7-6 | 0.15–0.21 % | 1.40–1.70 % | European twin of 4317 |
| 16MnCr5 | 0.14–0.19 % | — | Cheaper, shallower hardenability |
Supply Range and Delivery Condition
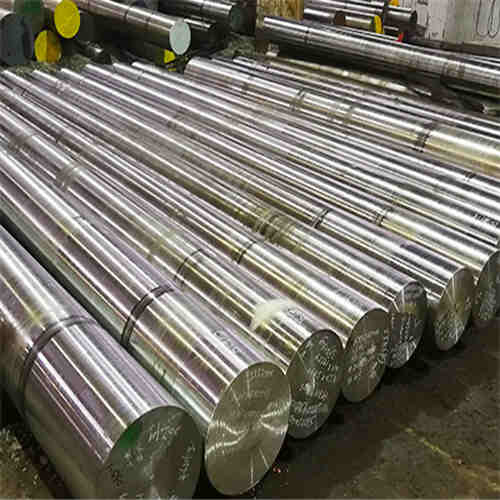
Supply is quoted by form and by delivered condition, because the same grade is bought annealed for machining or normalised for direct hardening.
Table 2 — Supply range by form, size and delivery condition
| Form | Size range | Delivery condition |
|---|---|---|
| Rolled round bar | Ø 16–300 mm | Annealed or normalised |
| Forged round bar | Ø 150–500 mm | Annealed |
| Forged flat bar | 100–400 × 300–1,200 mm | Annealed |
| Plate | 20–150 mm | Annealed |
Bar for gear cutting is supplied annealed to 200 HB maximum; bar for direct hardening is supplied normalised. The condition is on the certificate and decides the machining data.
Chemical Composition
The carbon range is deliberately low so the core stays tough; the alloy content is there to give the carburised case enough hardenability to survive the quench.
Table 3 — Chemical composition, wt. % (single values are maximums unless stated)
| Element | Min | Max | Typical |
|---|---|---|---|
| C | 0.15 | 0.21 | 0.18 |
| Si | — | 0.40 | 0.25 |
| Mn | 0.50 | 0.90 | 0.70 |
| P | — | 0.035 | 0.015 |
| S | — | 0.035 | 0.010 |
| Ni | 1.40 | 1.70 | 1.55 |
| Cr | 1.50 | 1.80 | 1.65 |
| Mo | 0.25 | 0.35 | 0.30 |
Mechanical Properties
Core properties are quoted in the delivered condition. Case properties are a function of the carburising cycle, not of the mill certificate alone.
Table 4 — Mechanical properties by condition
| Condition | Rp0.2 (MPa) | Rm (MPa) | A (%) | KV2 (J) | HB |
|---|---|---|---|---|---|
| Annealed | — | — | — | — | ≤200 |
| Normalised | ≥520 | 700–850 | ≥20 | ≥50 | 170–210 |
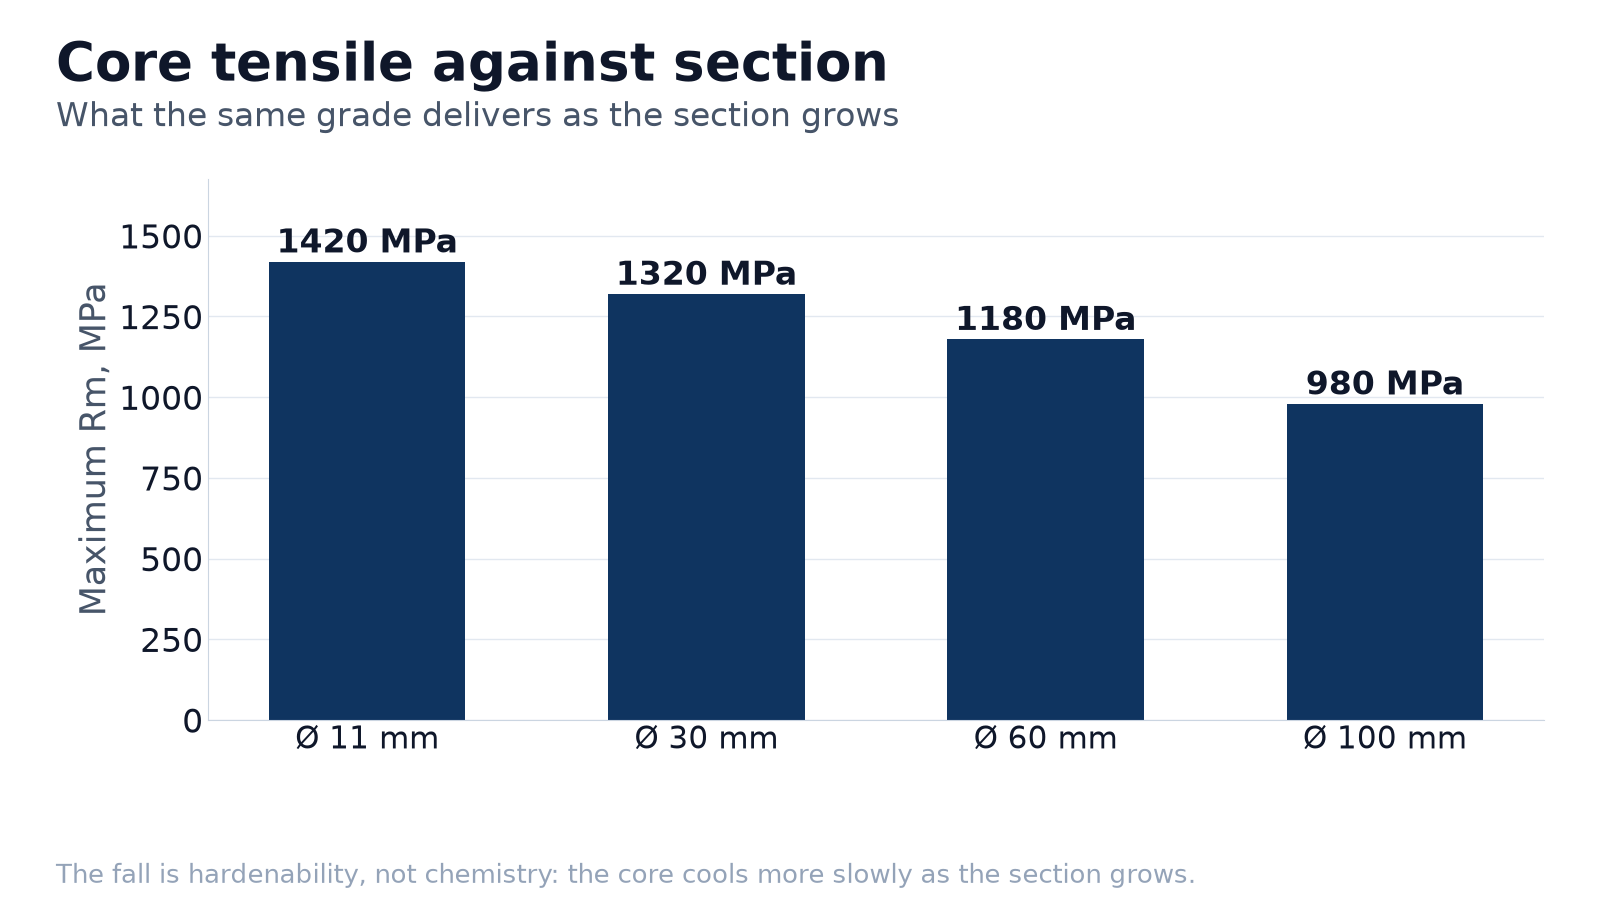
| QT, Ø ≤ 11 mm | ≥835 | 1,180–1,420 | ≥7 | ≥44 | 354–406 |
| QT, Ø 12–30 mm | ≥785 | 1,080–1,320 | ≥8 | ≥44 | 327–384 |
| QT, Ø 31–60 mm | ≥700 | 980–1,180 | ≥9 | ≥40 | 300–350 |
Heat Treatment
Carburise, quench and temper as one controlled sequence. The cooling rate through the case is what decides whether the surface reaches its full hardness.
Table 5 — Heat treatment schedule
| Step | Temperature | Time / atmosphere | Cooling |
|---|---|---|---|
| Carburising | 900–930 °C | 4–10 h, 1.0 % C potential | Furnace cool or direct quench |
| Austenitising for quench | 830–850 °C | 30 min | Oil |
| Tempering | 150–200 °C | 2 h | Air |
| Stress relief after rough machining | 600–650 °C | 2 h | Furnace cool |
Equivalent Grades and Standards
The Japanese and European designations overlap but do not align exactly on carbon and nickel. Check the analysis column before substituting one for the other.
Table 6 — Equivalent grades and governing standards
| System | Designation |
|---|---|
| AISI / SAE | 4317 / 4317H |
| UNS | G43170 |
| DIN | 1.6587 (18CrNiMo7-6) |
| EN | 18CrNiMo7-6 |
| GB | 17CrNiMo6 |
| JIS | SNC815 (close) |
What Ships With Every Lot
- EN 10204 3.1 mill certificate with chemistry and mechanical properties, heat number and melt route.
- Hardness survey and dimensional report on every piece on request.
- Ultrasonic inspection to ASTM A388 or SEP 1921 where the section or the application calls for it.
- Third-party inspection — SGS, BV, TUV — arranged before dispatch, at the customer’s instruction.
- Spectro check on the finished part where a weld or a heat treatment has been added after despatch.
Machining, Welding and Surface Finish
4317 machines in the annealed condition at 180–200 HB; the nickel makes it tougher under the tool than a plain chromium steel, so a rigid set-up and a positive rake are needed to avoid chatter on gear blanks.
Welding is not a normal route for a carburised gear. Where it is unavoidable, the weld is made before carburising, with preheat and a post-weld normalise, so that the weld responds to the case cycle like the parent metal.
Packing, MOQ and Delivery Terms
Bars are bundled and strapped, with the heat number and the condition on the tag. Gear blanks cut to length are packed in wooden cases with VCI paper.
Table 7 — Trade terms, packing and documents
| Item | Standard terms |
|---|---|
| Trade terms | FOB Shanghai / CIF / CFR / EXW; FOB is the default. |
| Minimum order | One bundle, plate or coil for stock sizes; mill runs quoted individually. |
| Lead time | 20–30 days from order confirmation for stock sizes; 30–45 days where forging or heat treatment is included. |
| Payment | 30 % T/T deposit, 70 % against the bill of lading copy; L/C at sight above 20 t. |
| Packing | Seaworthy export packing — crated or strapped, marked with grade, heat number, size and net weight. |
| Documents | EN 10204 3.1 certificate, packing list, invoice, bill of lading, certificate of origin; legalisation on request. |
Frequently Asked Questions
Is 4317 the same as 18CrNiMo7-6?
Close but not identical. The nickel and molybdenum ranges overlap; the phosphorus and sulphur limits differ. The comparison table above sets out the difference.
What case depth can I get?
0.3–1.5 mm effective case depth. The carburising time at 925 °C against depth is given on this page.
What core strength does it deliver?
1,180–1,420 MPa tensile in an 11 mm test piece, falling to 980–1,180 MPa at 31–60 mm.
Can it be supplied normalised?
Yes, and that is the usual condition for bar that will be carburised and quenched directly.
Do you supply to AISI or EN?
Both. The certificate names the specification and the edition used for the heat.
Related Grades
Browse the full range: alloy structural steel grades.
Request a Quote
- Grade and governing standard
- Form, size and quantity
- Delivery condition and hardness
- Certificate and testing requirements
- Destination port and required date
Email [email protected] or use the form below. Drawings in DXF, STEP or PDF are all fine. Stock sizes ship within 20 days of order confirmation.
