Short answer: pickling dissolves the contaminated surface layer; passivation rebuilds the chromium oxide film that makes the steel stainless. They are two different operations, usually specified together — and doing only the first is a common and expensive mistake.
Why stainless needs a film at all
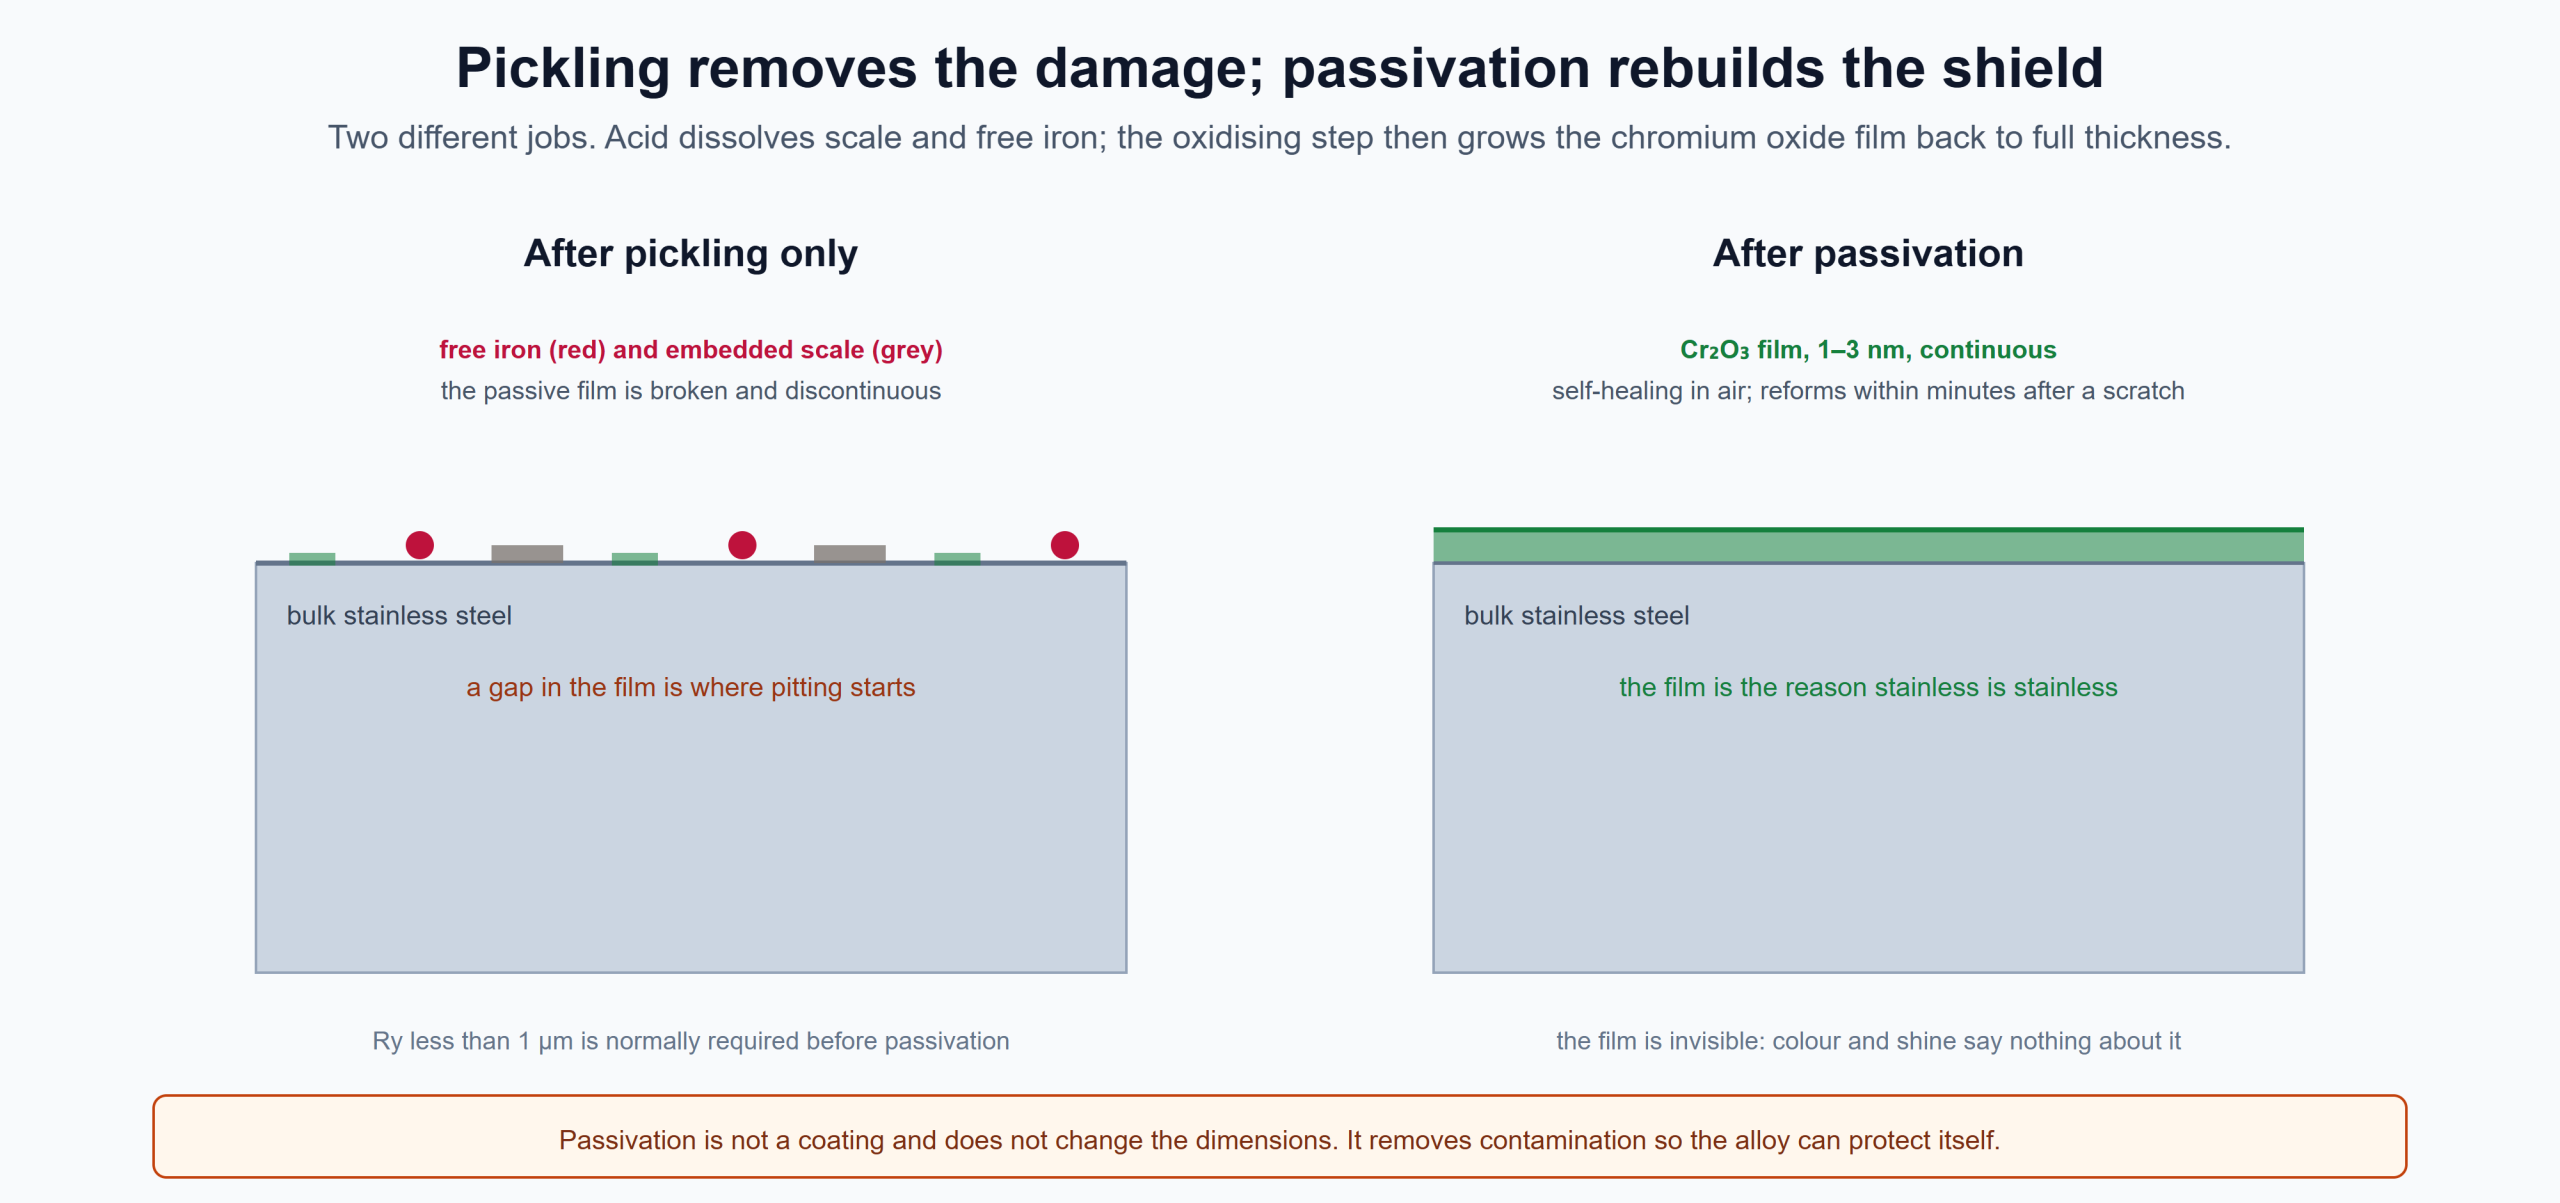
Stainless steel resists corrosion because of chromium, not because it is inert. Chromium oxidises preferentially at the surface and forms a chromium-rich oxide film roughly 1–3 nm thick. That film is what separates the steel from the environment; the bulk alloy behind it is only as good as the film covering it.
The film is also dynamic. It repairs itself in air within minutes after a scratch, which is why stainless steel is described as self-healing. But it is attacked by reducing conditions — chlorides above all — and it cannot repair itself under a layer of oil, scale or embedded iron. A surface that is contaminated is a surface that has no working film, whatever the certificate says about the chemistry.
What pickling removes
Pickling is an acid attack on the surface, and it removes four things that passivation cannot fix on its own: heat tint from welding and heat treatment, which is a chromium-depleted oxide; embedded free iron left by tooling, wire brushes and handling; sulphide and oxide inclusions smeared into the surface by machining; and the mechanically disturbed layer that carries residual strain.
Free iron is the one that matters commercially. It rusts first, in a spot that looks like a defect in the steel, and it is usually the reason a customer rejects a delivery that passed every mechanical test.
What passivation does
Passivation is the oxidising step that follows. Nitric acid at 20–25 % and 20–45 °C for 20–30 minutes is the classical formulation; citric-acid based products are used where nitric is restricted by the shop’s environmental permit or where the part has a complex geometry that traps acid.
The mechanism is selective dissolution: iron and iron oxides dissolve faster than chromium and chromium oxides, so the surface becomes chromium-enriched and the film that reforms on it is denser and more stable. The potential of that film approaches +1.0 V (SCE), which is why a properly passivated surface behaves closer to a noble metal than to carbon steel.
The methods, and which one fits the job
There are six practical routes, and the choice is driven by part geometry and by how much acid the shop is prepared to handle.
| Method | Fits | Limits |
|---|---|---|
| Dipping | Pipe, fittings, small parts, batch work | Needs an acid tank, heating and fume extraction; not for large fabrications |
| Paste | Weld seams, local repairs, site work | Labour intensive; poor operator environment; uneven on vertical surfaces |
| Spray | Tank interiors, fixed workstations | Needs continuous water and power; over-spray attacks adjacent steel |
| Circulation | Pipe systems, closed loops | Needs a pump and a temporary return; dead legs stay unpickled |
| Brushing | Touch-up after fabrication | Inconsistent; the brush itself can embed iron |
| Electrochemical | High-spec surfaces, electropolishing | Equipment and current control; not a site process |
Where it goes wrong
Most failures are not chemistry failures, they are sequence failures. The five that recur:
- Passivating a surface that is still oily. The acid cannot reach the steel, so nothing passivates and the oil is baked on instead.
- Chloride contamination. Tap water with more than about 50 mg/l chloride used for the final rinse leaves the film under attack from the moment it forms. Demineralised water is the fix.
- Over-pickling. Long immersion attacks the grain boundaries and can leave a smutted surface that is worse than the one you started with. It also introduces hydrogen, which matters on high-strength fasteners.
- Inadequate rinsing. Residual acid under a dried film shows up as a stain weeks later.
- No free-iron test. The ferroxyl test (potassium ferricyanide in a nitric acid solution, per ASTM A380) takes a minute and is the only check that actually proves the surface is clean.
What to write on the purchase order
Specify the standard, not the verb. ASTM A380 covers cleaning, descaling and passivation; ASTM A967 covers chemical passivation treatments with the specific times and temperatures; EN 2516 is the aerospace equivalent. Add the free-iron test, the maximum chloride content of the final rinse water, and the surface finish the part has to hold afterwards.
How the result is verified
Passivation is invisible, so acceptance depends on tests rather than on appearance. The set that matters is small:
- Free-iron test (ferroxyl). Potassium ferricyanide in dilute nitric acid turns blue where free iron sits on the surface. The result is visible in under a minute, and it is the check ASTM A380 describes for the purpose.
- Water-break test. A clean surface holds a continuous water film for about 30 seconds; oil, scale or contamination makes the film break into droplets. It is cheap, immediate, and most useful before passivation, as a check that the cleaning actually worked.
- Copper sulphate test. A drop of copper sulphate solution left for six minutes deposits copper where free iron is present. Common on pipe and tank work where a laboratory is not available.
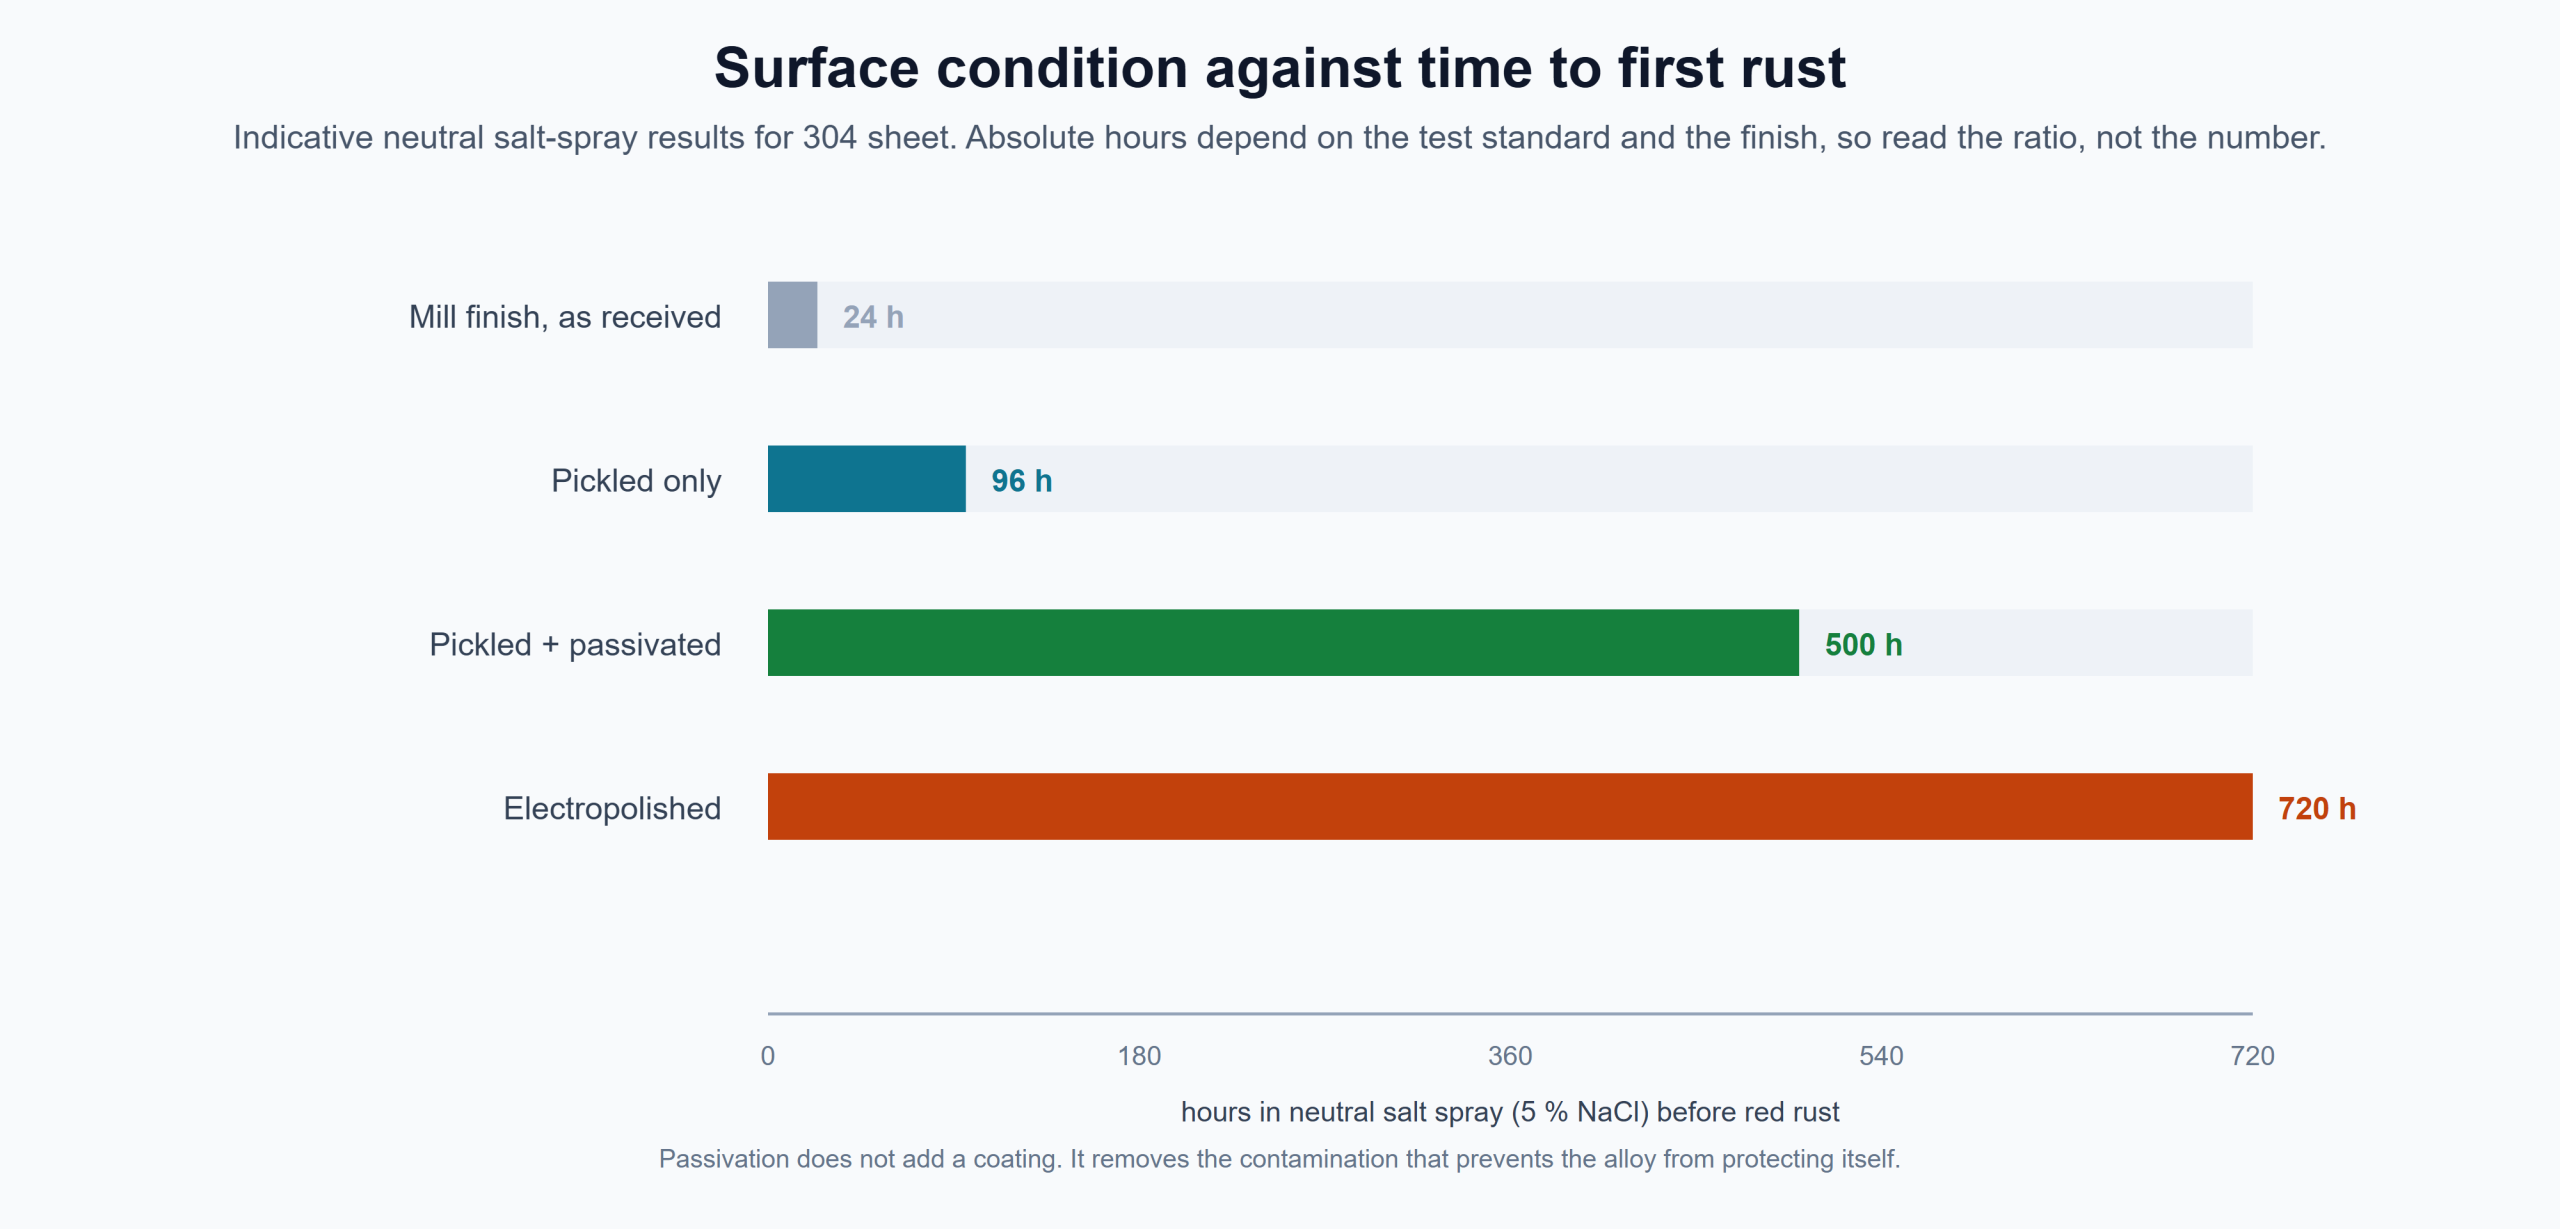
- Salt spray. ASTM B117 gives a comparative number, not an absolute service life. It is the test most often written into a purchase order and the least useful for predicting behaviour in a chemical tank.
None of these measures film thickness — the film is 1–3 nm and no shop-floor instrument sees it. The acceptance criterion is surface condition and the absence of free iron, not a number on a gauge.
Related reading
- Which stainless grades are magnetic — the same chromium film, seen from the magnetic side.
- 317L stainless steel — the grade specified when chlorides are the problem.
- The 400 series — martensitic grades that passivate differently from the austenitic ones.
- Steel hardness conversion chart — if the part is also hardness tested, do not convert across methods.
- Non-destructive testing types — penetrant inspection after passivation, and why the sequence matters.
You get chemical composition, mechanical properties and a price — with inspection certificates to EN 10204 3.1 issued against the heat number.