What Is Quenching? Definition, Media and Cooling Rates Explained
The definition in one sentence, the martensite transformation that makes it work, how air, oil, water, brine and polymer differ in cooling rate, and why quenching without tempering is a rejected part waiting to crack.
Quenching is the rapid cooling of a steel part from its austenitizing temperature in order to suppress the diffusion-controlled transformations and force the austenite to transform into martensite or bainite. That sentence is the answer most people are looking for. Everything below it is the detail that decides whether the quench produces a hard, sound part or a cracked one.
The word is used loosely in industry. In a tool room it usually means an oil or water quench from 1000 °C or above, followed by tempering. In a stainless steel mill it means a water spray after solution annealing at 1050 °C, where the purpose is not to harden but to keep alloying elements in solution and prevent sensitization. Both are quenching; the metallurgical objective is different, and confusing them is a common source of bad specifications.
Why Quenching Hardens Steel: The Martensite Transformation
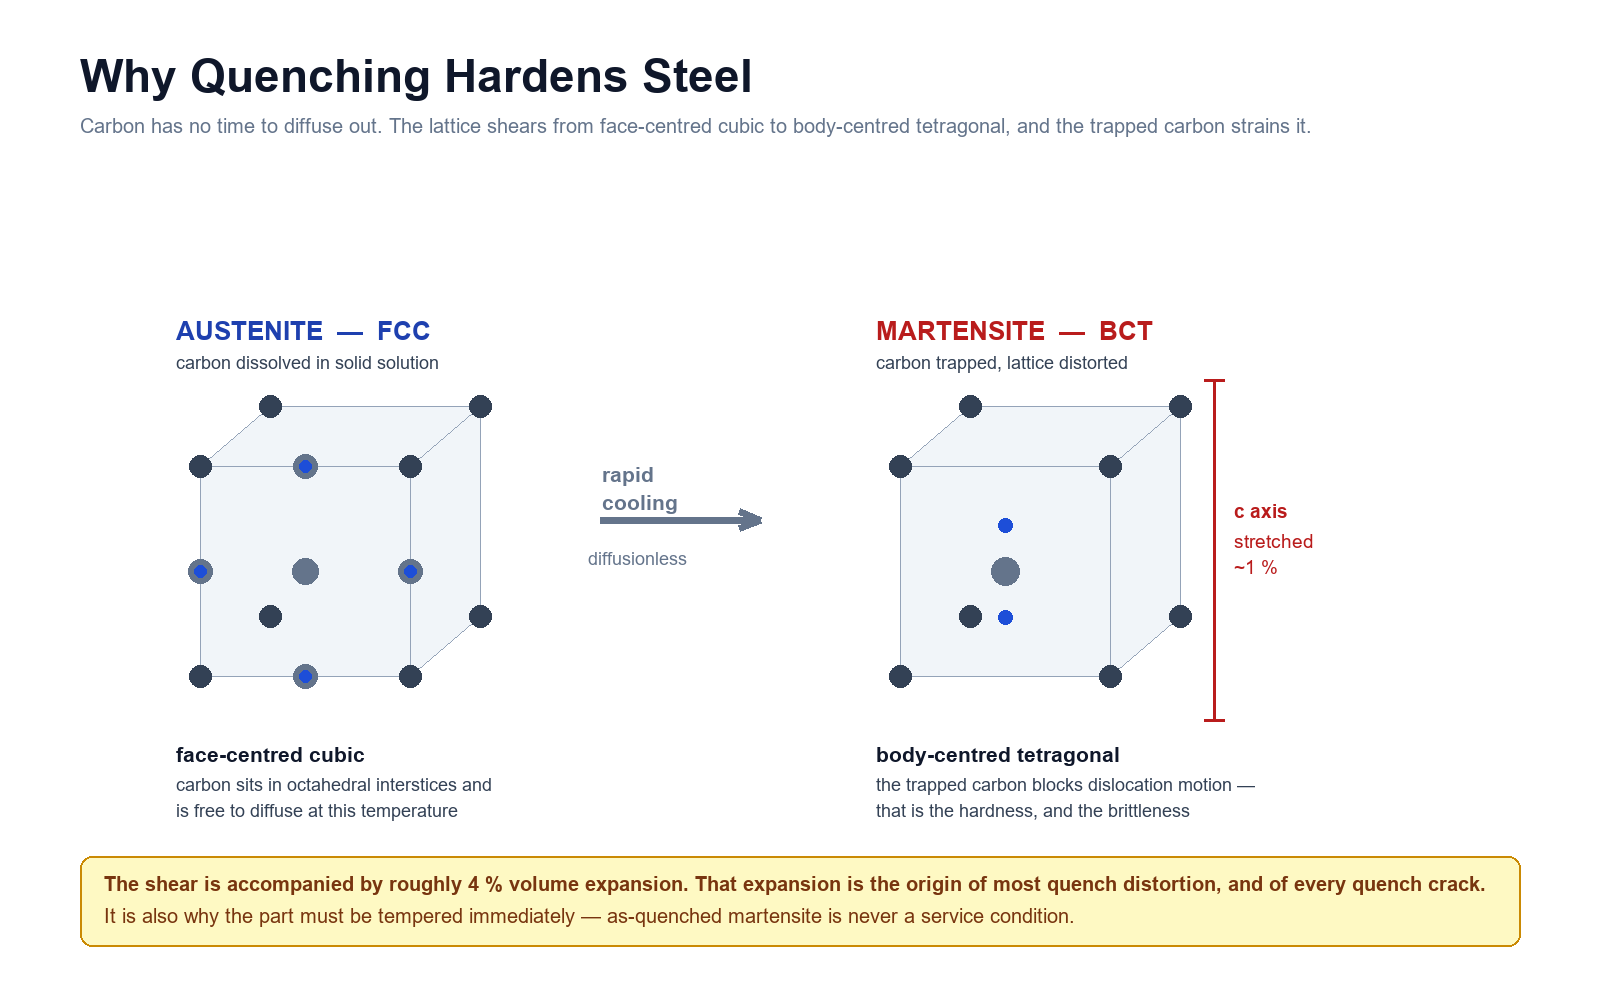
Above the Ac3 line, steel is austenite — a face-centred cubic structure with carbon dissolved in solid solution. If it cools slowly, carbon has time to diffuse out and the steel transforms into ferrite and pearlite at comparatively high temperature, which is soft. If it cools fast enough, the carbon is trapped.
The transformation then happens without diffusion, by a shear mechanism: the face-centred cubic lattice collapses into a body-centred tetragonal one, with the excess carbon held in supersaturated solution. The result is martensite, and its hardness comes from that trapped carbon — the tetragonal distortion strains the lattice and blocks dislocation movement. A 0.4 % C steel quenched to full martensite reaches roughly 55–58 HRC from a soft annealed condition near 200 HB.
Two consequences follow. First, the transformation is accompanied by a volume increase of about 4 %, which is the origin of most quench distortion and quench cracking. Second, martensite is hard but brittle, and the as-quenched condition is never a service condition — it must be tempered.
The Quenching Media
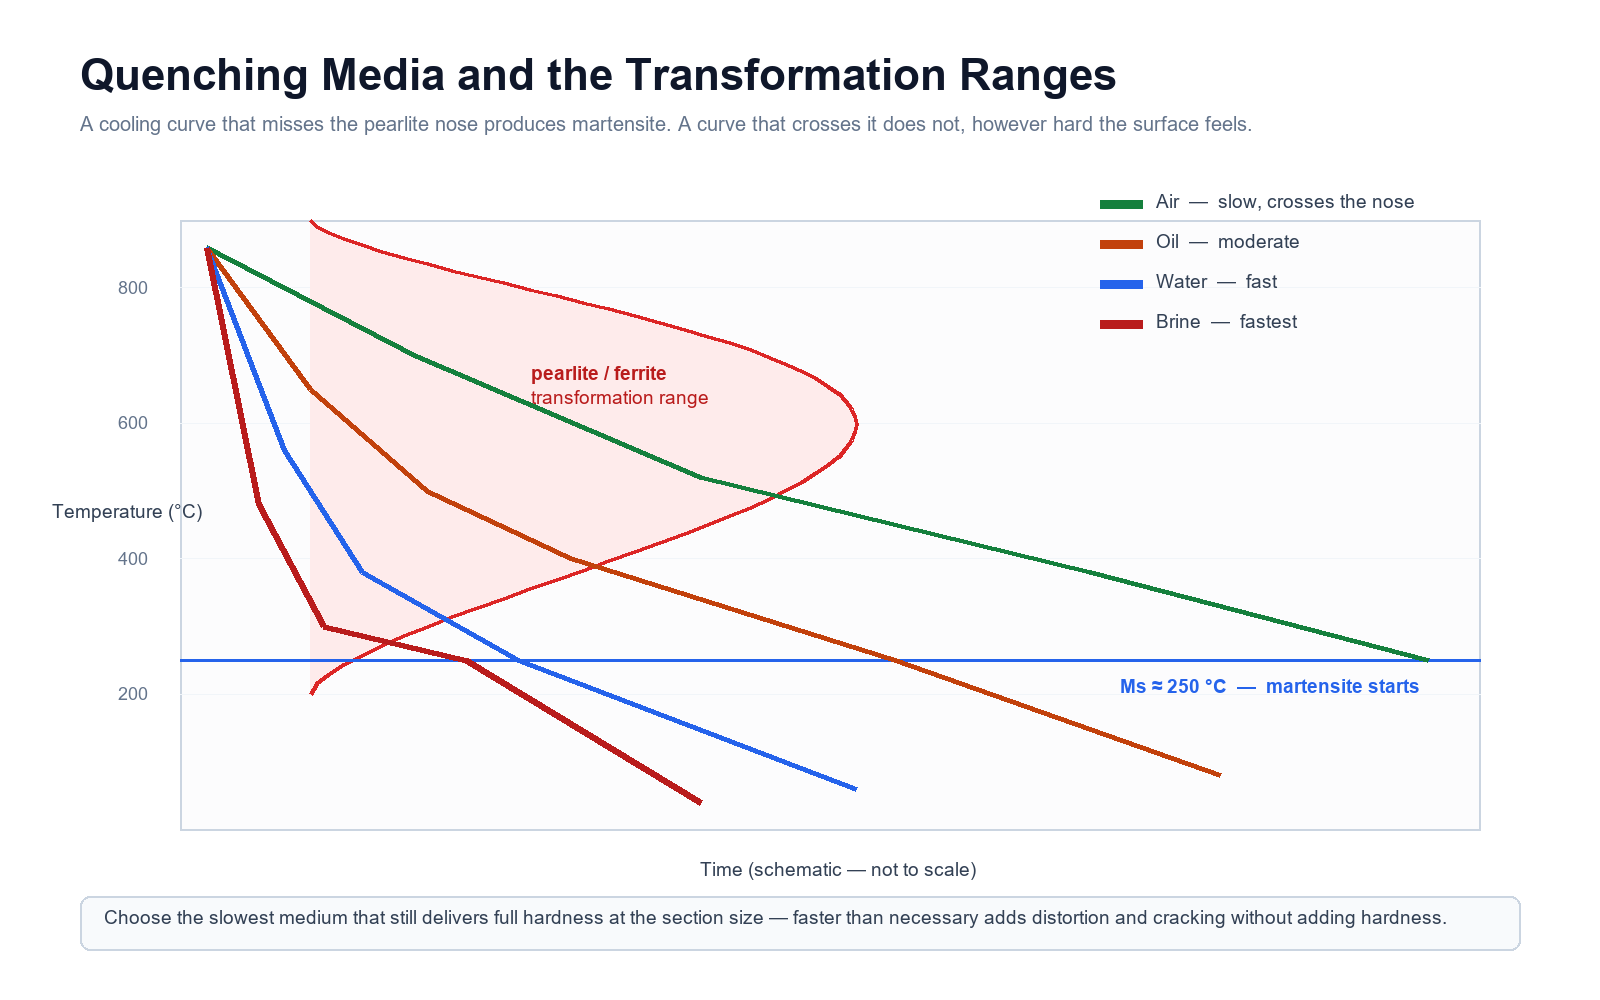
The medium only matters to the extent that it controls the cooling rate in the temperature range where transformation decisions are made — roughly 800 °C down to 300 °C. Cooling speed at the top of that range decides whether martensite forms at all; cooling speed at the bottom decides how much stress the part carries.
| Medium | Cooling rate at 700 °C (approx.) | Hardening power | Typical use | Main risk |
|---|---|---|---|---|
| Still air | 1–5 °C/s | Very low | Air-hardening tool steels (A2, D2), large sections | Insufficient hardness in thick sections |
| Forced / compressed air | 5–20 °C/s | Low | Vacuum furnace loads, H13 dies | Uneven cooling between thin and thick sections |
| Oil | 10–30 °C/s | Moderate | Alloy and tool steels, gears, shafts | Fire, smoke, surface oxidation; temperature-dependent viscosity |
| Water | 30–100 °C/s | High | Plain carbon steels, induction-hardened surfaces | Vapour blanket stage, soft spots, cracking |
| Brine | 100–200 °C/s | Very high | Low-hardenability carbon steels, case-hardened parts | Corrosion of equipment; severe cracking risk |
| Polymer solution | Tunable, 5–80 °C/s | Adjustable | Replacement for oil and water; induction lines | Concentration drift, biological degradation |
Table 1 — Quenching media. Cooling rates are indicative for still, unagitated conditions; agitation raises them substantially, particularly for oil.
The ranking is not a ranking of quality. A water quench is not better than an oil quench — it is faster, and faster is only useful when the steel needs it. Choose the slowest medium that still delivers full hardness at the section size in question; anything faster adds distortion and cracking risk without adding hardness.
This is the single most common specification error in heat treatment. A 4140 shaft quenched in water because the shop has always used water will often crack at a section change; the same shaft in oil reaches the same core hardness because 4140 has enough hardenability. Conversely, a plain 1045 part quenched in oil may come out with a soft ferrite network because the oil cannot outrun the pearlite transformation at that section size.
The Critical Cooling Rate
Every steel has a critical cooling rate: the slowest cooling that still avoids the pearlite and bainite noses on the continuous cooling transformation diagram. Cool faster and the structure is martensitic; cool slower and it is not, regardless of what the hardness file says the steel is capable of.
The critical rate falls steeply as alloy content rises. A plain 0.8 % carbon steel needs several hundred degrees per second and is effectively water-quench only. Adding chromium, molybdenum and nickel pushes the transformation curves to the right, so a 1.5 % Cr–Mo tool steel can harden in still air. That is precisely what hardenability means, and it is measured rather than calculated — by the Jominy end-quench test to ASTM A255, or by the ideal diameter method.
Practical consequence: critical cooling rate is a property of the grade, while actual cooling rate is a property of the medium, the section size and the agitation. Hardening succeeds when the second exceeds the first at every point in the section that the drawing requires to be hard.
Quenching Methods Used in Practice
Direct immersion quench. The part is transferred from the furnace to the tank and held until it reaches bath temperature. Simple and fast, but the transfer time matters — more than about five seconds produces a temperature drop that can start transformation before the part is even in the oil.
Interrupted quench. The part is cooled in the medium until just above the martensite start temperature, withdrawn, and allowed to equalize before final cooling. It reduces the thermal gradient through the section and therefore reduces distortion, at the cost of a more demanding process window.
Martempering (step quench). The part is quenched into a salt or oil bath held just above the Ms temperature, held until the section is uniform, then cooled in air. Martensite forms slowly and uniformly, which minimizes distortion and cracking. It does not reduce hardness.
Austempering. The part is quenched into a bath held between the Ms and the bainite finish temperature and held until the transformation to bainite is complete. It produces a tough, ductile structure without a subsequent temper, and is used for springs, wire and thin sections.
Spray and induction quenching. Cooling is applied locally, usually immediately after induction or flame heating. It hardens a selected surface rather than the whole section, and is the standard route for shaft journals, gear teeth and cam lobes.
Distortion, Cracking and Residual Stress
Two stresses act during a quench. Thermal stress arises because the surface cools and contracts before the core, putting the surface in tension. Transformation stress arises because martensite forms later in the core, and its volume expansion pushes outward against an already-hard shell. When the two combine at a stress concentration — a sharp fillet, a keyway, a drilled hole, a thread root — the part cracks.
The practical countermeasures are well established. Design out sharp section changes. Use the slowest medium that still hardens the part. Agitate uniformly and orient the part so that cooling is symmetrical. Quench a part with a bore from the outside in, and plug blind holes. Round all edges before quenching, because an edge is a stress raiser with no material behind it.
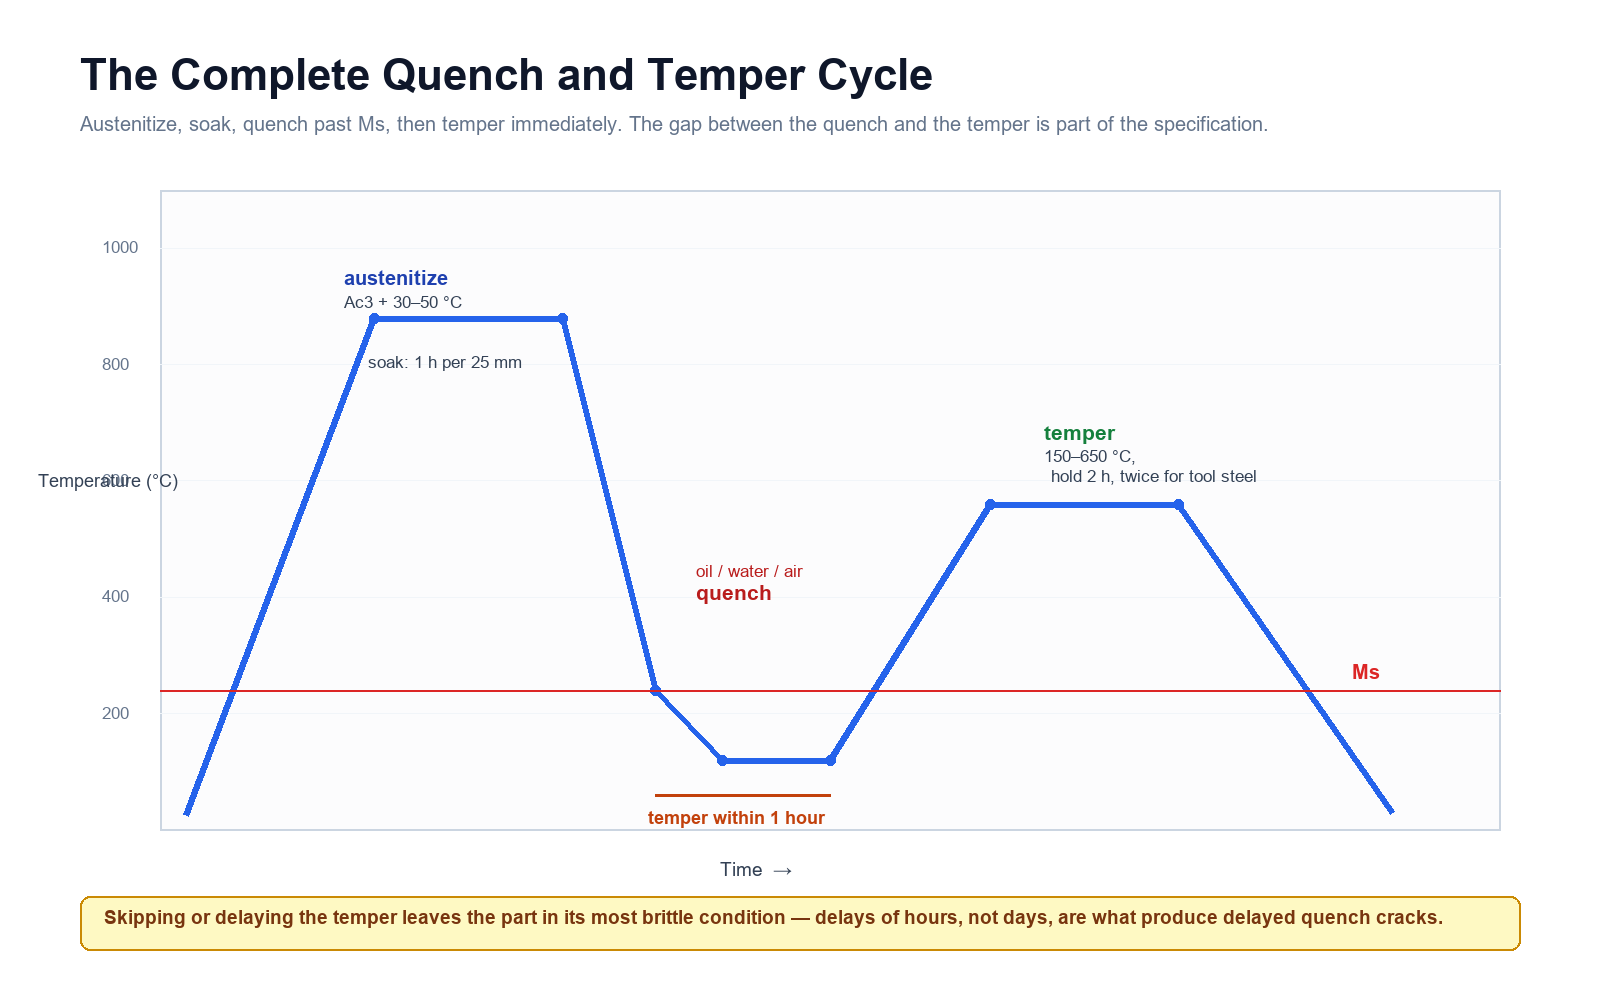
Cracks that appear hours after the quench rather than immediately are usually hydrogen-related or the result of delayed transformation, and they are the reason the tempering interval is specified in hours rather than days.
Tempering: What Must Follow
As-quenched martensite is too brittle to use. Tempering reheats the part, usually between 150 °C and 650 °C, to allow carbon to precipitate as fine carbides, relieving internal stress and trading hardness for toughness in a controlled way.
Three rules are worth committing to memory. Temper immediately — for most alloy and tool steels, within one hour of the quench, and never overnight. Temper twice for tool steels and for any part with a large section change, because retained austenite transforms during the first temper and needs a second cycle to be addressed. Stay below the secondary hardening peak unless you are deliberately using it — for high-speed steels the peak near 550 °C is intentional, but for structural steels it is a brittleness range to be avoided.
The temperature determines the result far more than the time. A part tempered at 200 °C for four hours will still be harder than the same part tempered at 400 °C for one hour. If a hardness specification cannot be met, the tempering temperature is the variable to change, not the soak time.
Typical Cycles for Common Grades
The numbers below are working starting points for the grades most often bought in quenched and tempered condition. They are not substitutes for the material supplier’s recommendation or for a procedure qualified on the actual section size — a 25 mm bar and a 250 mm forging of the same grade do not run the same cycle.
| Grade | Austenitizing | Quench medium | Temper | Typical hardness |
|---|---|---|---|---|
| 1045 / C45 | 820–850 °C | Water or brine | 550–660 °C | 25–32 HRC |
| 4140 / 42CrMo4 | 840–870 °C | Oil | 540–680 °C | 28–36 HRC |
| 4340 / 36CrNiMo4 | 830–860 °C | Oil | 540–660 °C | 30–38 HRC |
| H13 / 1.2344 | 1000–1030 °C | Air or oil, or vacuum gas | 500–600 °C, twice | 45–52 HRC |
| D2 / 1.2379 | 1010–1040 °C | Air or oil | 180–250 °C, twice | 58–62 HRC |
| M2 / 1.3343 | 1190–1230 °C | Oil, air or salt | 540–560 °C, three times | 63–66 HRC |
| 420 / 1.4021 | 980–1050 °C | Oil or air | 200–350 °C | 48–54 HRC |
Table 2 — Typical quench and temper cycles. Tool steels are tempered two or three times to address retained austenite; structural steels usually once.
Note how the medium tracks the grade rather than the hardness target. 1045 needs brine because it has almost no alloying element to slow the transformation; H13 hardens in still air because 5 % chromium and 1.5 % molybdenum already do that job. Selecting a medium by “how hard we want it” rather than by hardenability is how cracked parts get made. Our tool steel and AISI 4140 alloy steel pages carry the full analysis limits for these grades.
Quenching Stainless Steels and Nickel Alloys
In austenitic stainless steel, quenching follows solution annealing at 1040–1120 °C and has nothing to do with hardness. The purpose is to cool fast enough through the 850–450 °C sensitization range to prevent chromium carbide precipitation at the grain boundaries, which would leave the steel vulnerable to intergranular corrosion. Water quenching or forced-air cooling is standard; a slow furnace cool is a defect, not a process variant.
Martensitic and precipitation-hardening grades behave more like alloy steel. 410 and 420 harden by quench and temper; 17-4PH is solution treated then aged, and the cooling rate after solution treatment controls the amount of retained austenite and therefore the final properties. Nickel-based alloys such as Inconel 718 are solution treated and aged, with the quench again used to hold elements in solution rather than to harden. Our notes on Inconel 718 forging and heat treatment cover that cycle in detail.
How Quenching Is Specified on a Purchase Order
A specification that says only “quenched and tempered” leaves the outcome to the supplier. The minimum useful statement covers five items: the austenitizing temperature and soak time, the quenching medium, the tempering temperature and the number of tempers, the required hardness range and test location, and the required microstructure if it matters.
For anything with a hardenability requirement, add the Jominy limit or the ideal diameter. For anything with a distortion allowance, add the permitted dimensional change and the straightening operation. And for anything that failed in service, ask for the actual cooling curve rather than the nominal procedure — the difference between the two is where most quench problems live. Our overview of annealing, normalizing and hardenability sets out how the four core processes divide the work, and the steel hardness conversion chart is useful for checking a certificate against the drawing.
Frequently Asked Questions
What does quenching mean in simple terms? Heating steel to a high temperature and cooling it very quickly, usually in oil or water, so that it becomes hard. The fast cooling traps carbon in the crystal structure, and that trapped carbon is what makes the steel hard.
What is the difference between quenching and tempering? Quenching hardens and embrittles; tempering reheats the part to relieve stress and restore toughness. They are two halves of one process and are almost never specified separately.
Can you quench stainless steel? Austenitic grades are quenched after solution annealing to prevent sensitization, not to harden. Martensitic grades such as 410 and 420 are genuinely hardened by quenching.
What happens if you quench too fast? Distortion and cracking, particularly at section changes and sharp corners. Faster than necessary adds no hardness once the critical cooling rate is exceeded — it only adds stress.
Why is oil used instead of water? Oil cools more slowly, which is gentler on alloy steels that do not need a water-quench rate. Using water on a steel that hardens in oil turns a sound part into a cracked one for no benefit.
What We Supply
Fushun Special Steel supplies tool steel, alloy steel, stainless steel and nickel alloys in the heat-treatment condition specified on the order — annealed, normalized, quenched and tempered, or solution treated — with hardness survey and microstructure report where required. If a part has failed after heat treatment, send us the grade, the section size and the cycle, and we will identify whether the cooling rate, the medium or the tempering step is responsible.
You get chemical composition, mechanical properties and a price — with inspection certificates to EN 10204 3.1 issued against the heat number.