
What Is Case Hardening? Four Processes, One Principle
A hard surface over a tough core. Every case hardening process achieves that in a different way, at a different temperature, with a different case depth — and the differences decide which one belongs on your drawing.
Case hardening is not one process. It is a family of four, and the family name hides the fact that they work at temperatures almost 400 °C apart and produce cases from 0.1 mm to 5 mm deep. Choosing between them is a question of case depth, distortion tolerance and the steel you already have.
The principle: a hard case on a tough core
A part that has to resist wear and survive impact wants two contradictory things from one material: a surface hard enough not to wear, and a core tough enough not to shatter. Through-hardening forces a compromise. Case hardening removes it: the surface is enriched or transformed, the core is left alone, and the two are joined by a gradient rather than a step.
That gradient is the thing to specify. A case that is too shallow will collapse under load — the classic failure of a carburised gear tooth that spalls after a few thousand hours. A case that is too deep is brittle and expensive. The right depth is a function of load, contact geometry and the core hardness underneath.
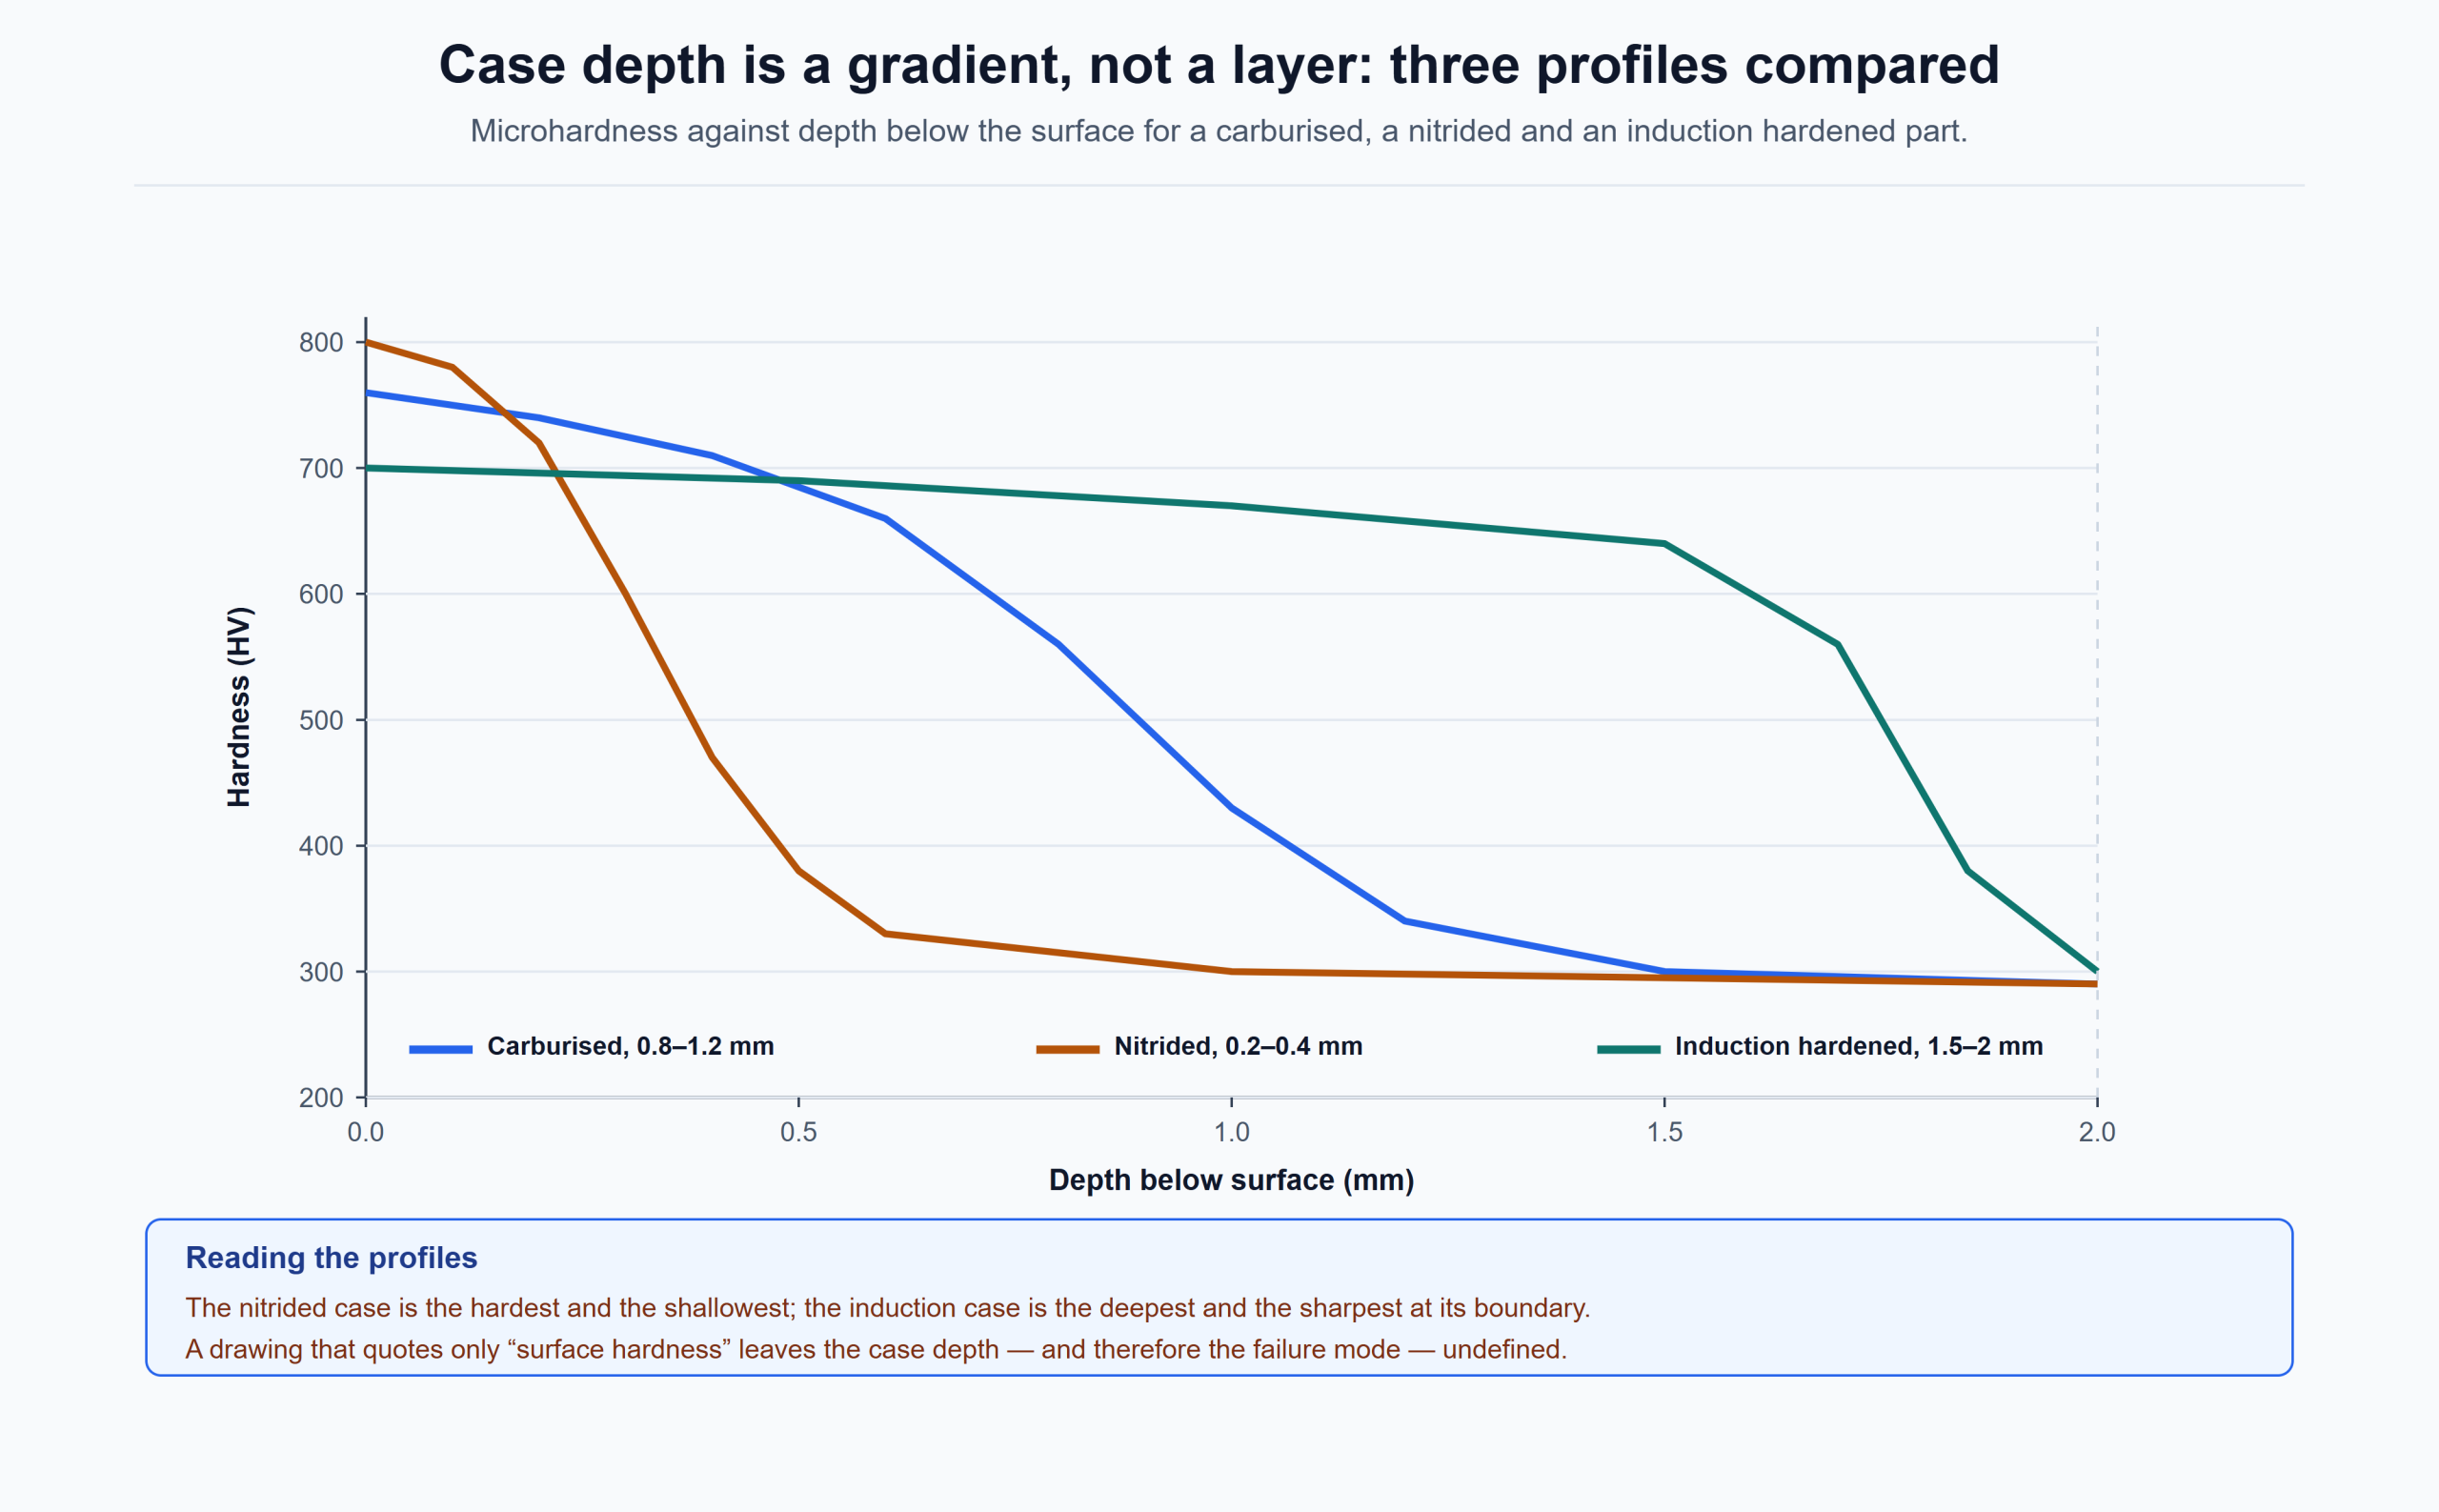
The four processes compared
Table 1. The four case hardening processes, their working temperature, typical case depth and the steel each one needs.
| Process | Temperature | Medium | Case depth | Distortion | Steel |
|---|---|---|---|---|---|
| Carburising | 880–950 °C | Gas, pack or salt; carbon | 0.3–2.0 mm | Moderate; quench required | Low carbon, 0.15–0.25 % C |
| Carbonitriding | 820–880 °C | Gas with ammonia; C and N | 0.1–0.75 mm | Moderate; quench required | Mild and low-alloy steel |
| Nitriding | 500–570 °C | Ammonia gas or plasma; nitrogen | 0.1–0.6 mm | Very low; no quench | Steel with Cr, Mo, Al or V |
| Induction or flame | Surface above 850 °C | No medium; heat then quench | 0.5–5 mm | Low, and local to the heated band | 0.35–0.55 % C steel |
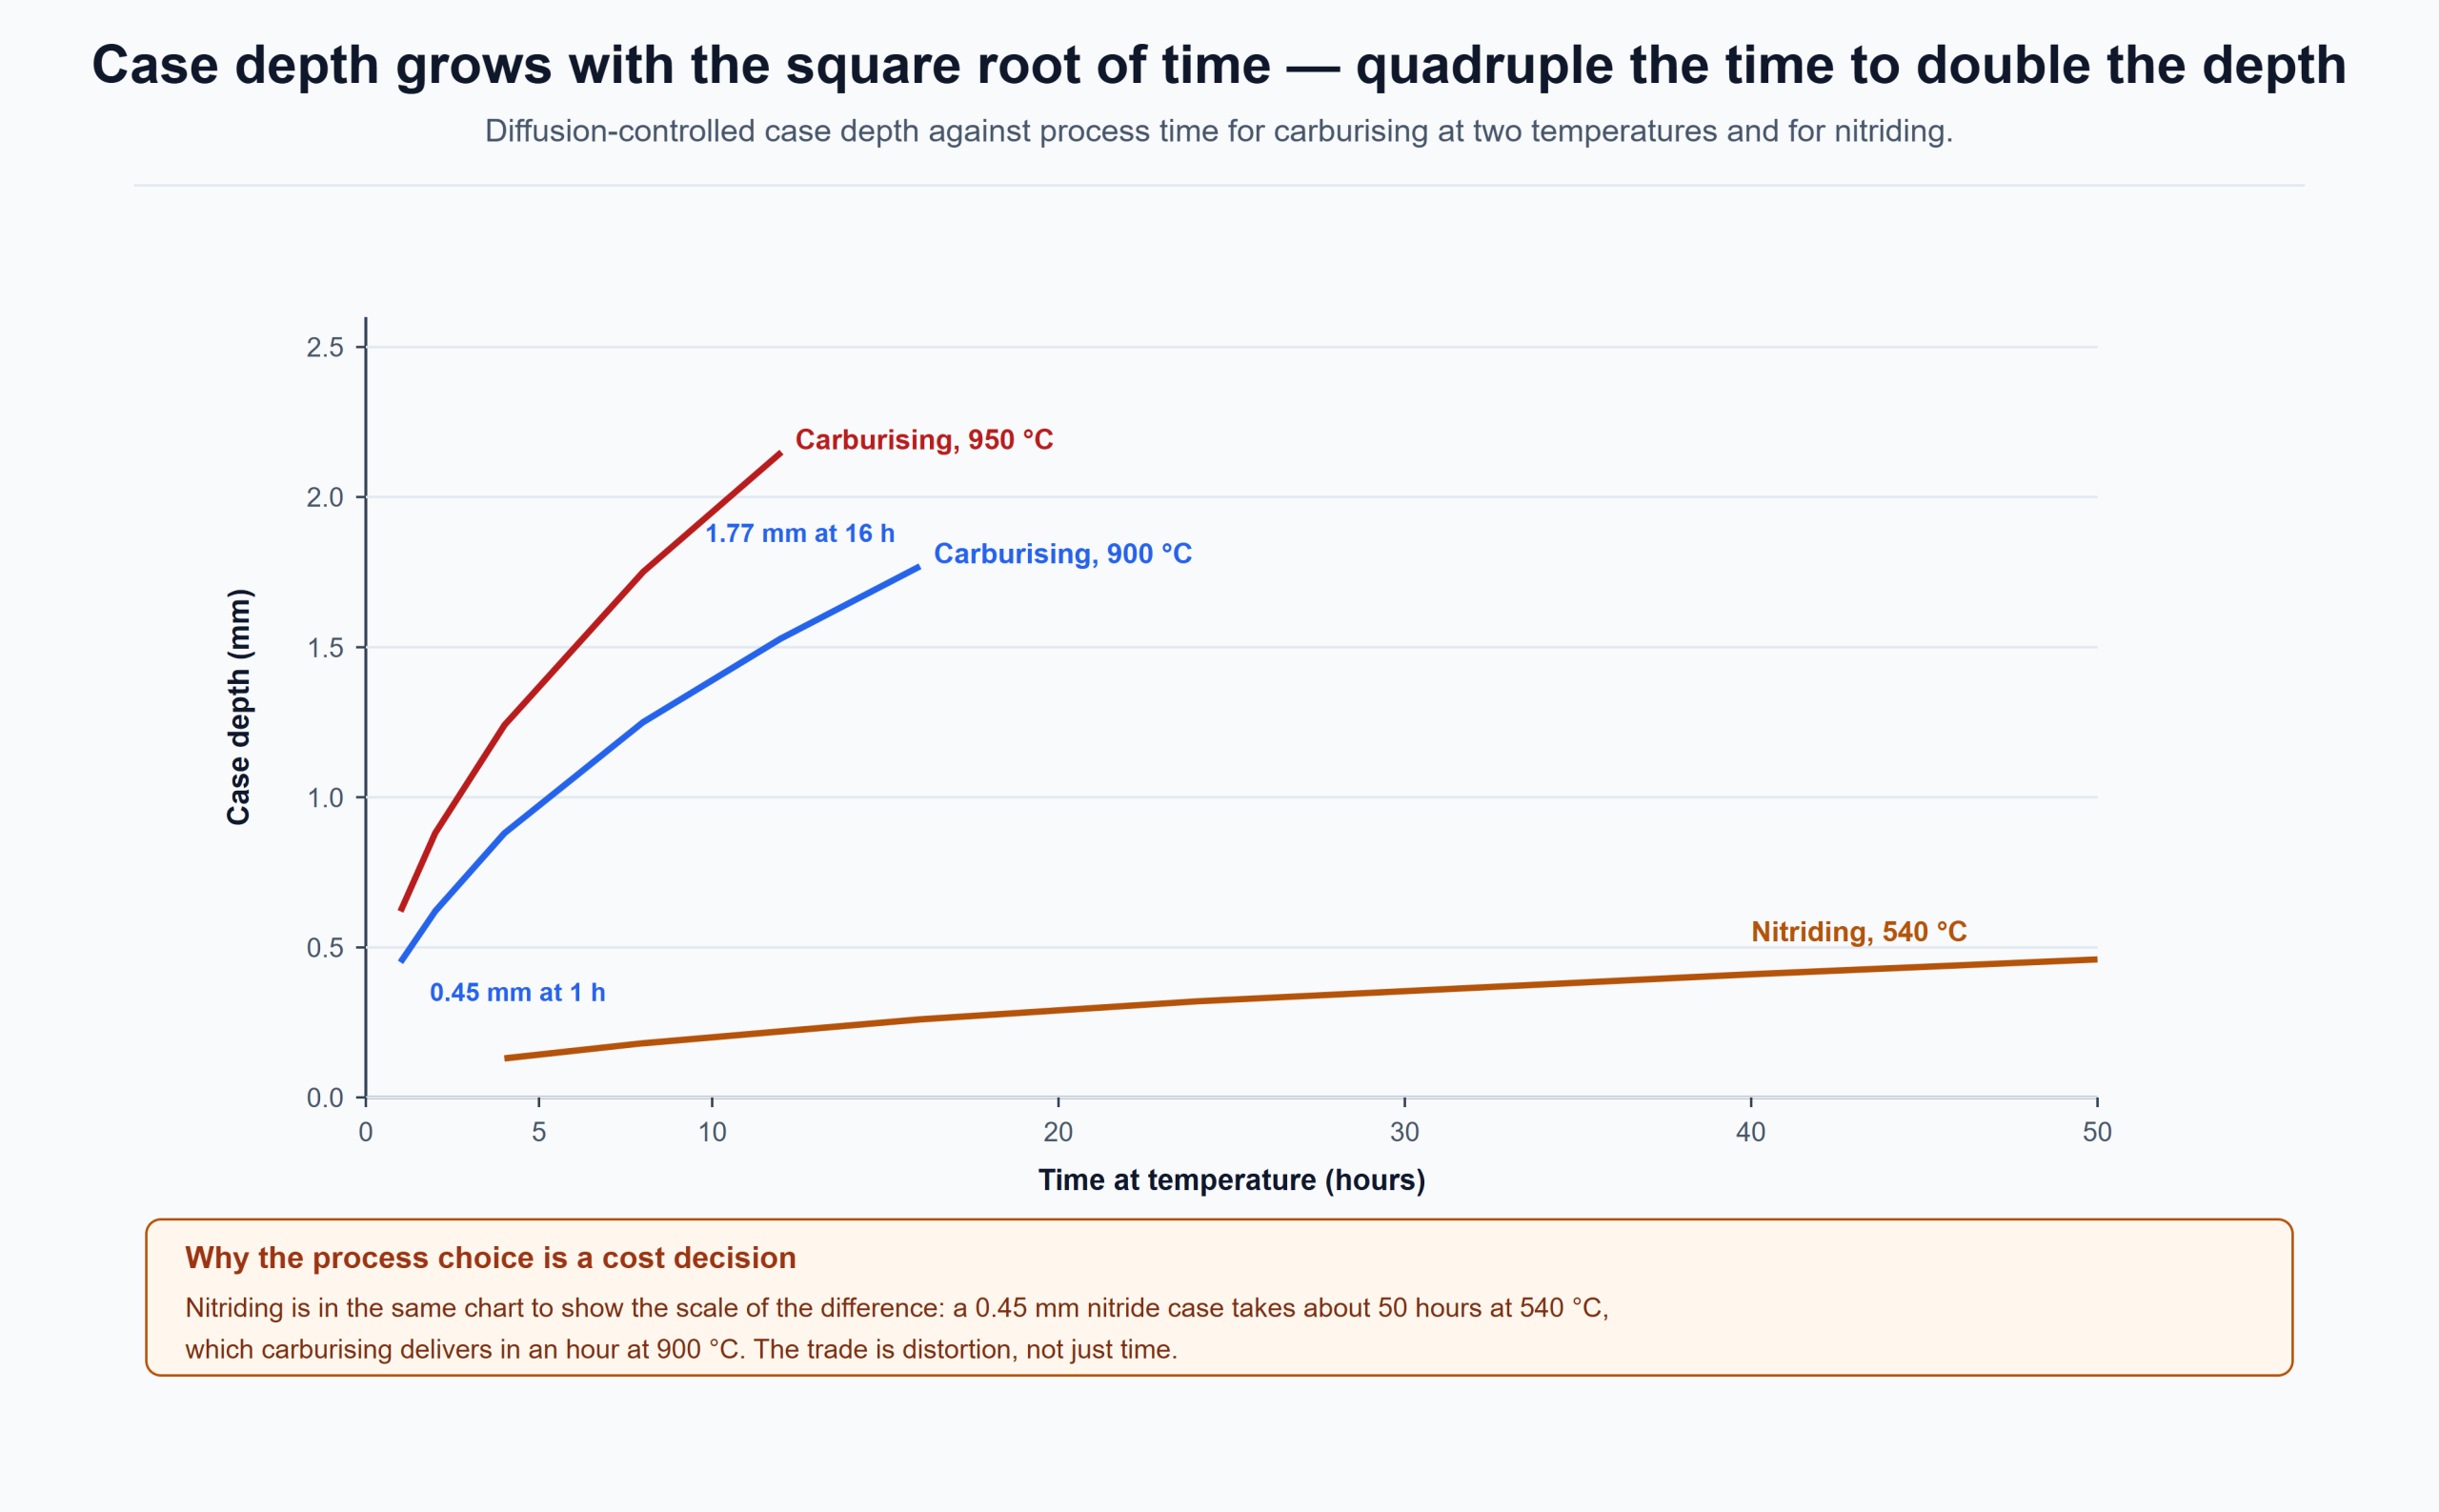
The two diffusion processes, carburising and nitriding, are often confused because both harden a surface without melting it. They are not interchangeable. Carburising puts carbon in at 900 °C and then quenches, so it needs a low-carbon steel and accepts distortion. Nitriding puts nitrogen in at 540 °C and never quenches, so it needs a steel containing nitride formers and produces almost no distortion — but it takes tens of hours to build a case that carburising builds in four.
Carburising
The part is held in a carbon-bearing atmosphere at 880–950 °C. Carbon diffuses into the surface until the outer layer reaches roughly eutectoid composition, and the part is then quenched — directly from the furnace, or after a reheating step that refines the grain. The result is a martensitic case at 58–62 HRC over a core that stayed low carbon and therefore stayed tough.
The steel has to start low in carbon: 0.15–0.25 % is typical, which is why 18CrNiMo7-6, 17CrNiMo6 and the 8620 family exist. A medium-carbon steel cannot be carburised to advantage, because the core would harden too and the toughness the process is bought for would be lost.
Nitriding
Nitriding does not add carbon and does not quench. Ammonia (or a plasma) supplies nitrogen at 500–570 °C, and the nitrogen reacts with chromium, molybdenum, aluminium and vanadium in the steel to form hard nitride particles. The case is typically 0.1–0.6 mm deep, harder than a carburised case (often above 700 HV), and it keeps its hardness to about 500 °C — which is why nitrided parts are used in hot and abrasive service.
The absence of a quench is the commercial point: a nitrided gear or extrusion screw comes out straight. The cost is time. A 0.4 mm case takes 30 hours or more, and the process only works on steels that contain the nitride formers — 4140 will nitride, 1045 will not to any useful depth.
Carbonitriding
Carbonitriding sits between the two: carbon and nitrogen are introduced together at 820–880 °C, followed by a quench. The nitrogen raises hardenability, so the case forms in a cheaper, lower-alloy steel and at a lower temperature than carburising, with less distortion. Case depths are shallow — 0.1–0.75 mm — which makes it a process for small parts: fasteners, pins, bushes and thin-section components.
Induction and flame hardening
These are not diffusion processes at all. The surface is heated above the austenitising temperature by an induction coil or a flame, then quenched, so the case is formed from the steel’s own carbon. It is fast — seconds rather than hours — and it can be applied to a single band on a shaft, which is why induction hardening is used for bearing journals, splines and gear teeth.
The steel needs 0.35–0.55 % carbon to respond, and the case depth is set by frequency rather than time: high frequency gives a shallow case, low frequency a deep one. There is no diffusion gradient, so the transition from case to core is sharper than in a carburised part — an advantage in wear, a disadvantage in fatigue if the transition is badly placed.
How deep, and how long
Case depth in a diffusion process grows with the square root of time, so doubling the depth takes four times as long. That single relationship explains most of the cost difference between a 0.5 mm and a 1.5 mm case, and it is the reason a drawing that specifies “case 1.5 mm minimum” without a load case is worth challenging.
Which process for which part
- Gears and shafts carrying high contact load: carburise. The deep case and the tough core are what resist pitting and tooth-root bending.
- Parts that must stay straight: nitride. No quench means no distortion, and the case keeps its hardness hot.
- Small fasteners, pins and bushes: carbonitride. Shallow case, cheap steel, low temperature.
- A band on a finished shaft: induction harden. It is the only one of the four that can be applied locally after machining.
- Stainless and tool steels: nitride, if at all. Carburising a stainless steel destroys the chromium oxide layer the grade was bought for.
What to put on the drawing
- Effective case depth, with a method: to 550 HV, or to 0.4 % carbon, or to a stated hardness. “Case hardened” alone is not a specification.
- Surface hardness, and the core hardness required underneath it. A hard case on a soft core will collapse.
- The areas to be left soft, and the masking method. Threads, keyways and seal surfaces are usually protected.
- Distortion allowance and the finishing operation after hardening. Most case hardening is done before final grinding, not after.
- The acceptance test: microhardness traverse on a sectioned coupon, or a hardness file test at a stated load.
Which steels can be case hardened
Case hardening is a ferrous process. Carburising and carbonitriding need low-carbon steel; nitriding needs chromium, molybdenum, aluminium or vanadium in the analysis; induction hardening needs enough carbon to transform. The common choices are the case-hardening alloy steels — 18CrNiMo7-6, 17CrNiMo6, 20NiCrMo2 and the 8620 family — for carburising, and the nitriding steels — 31CrMoV9, 34CrAlNi7 — for the lower-temperature route. Cast irons and some stainless grades can be nitrided; titanium and aluminium alloys are special cases.
Supply is normally annealed or normalised for machining, with the case-hardening response guaranteed by the hardenability band rather than by the chemistry alone. Where the part is safety-critical, the certificate should carry the Jominy or hardenability data for the heat, not just the composition.
Related reading
- 18CrNiMo7-6 case-hardening steel — the standard carburising steel for gears and shafts
- 31CrMoV9 nitriding steel — the reference grade for a deep, hard nitride case
- 34CrAlNi7-10 — aluminium-bearing nitriding steel for the hardest cases
- AISI 4140 — the through-hardening grade that is also widely nitrided
- What is quenching — the cooling step behind every quenched case
You get chemical composition, mechanical properties and a price — with inspection certificates to EN 10204 3.1 issued against the heat number.
